THE ROLE OF AN FTTH CABLE PRODUCTION LINE IN FIBER OPTICS

Intermittent Bonded Ribbon Production Line Available For Sale

A specified speed of 600 m/min gives this equipment considerable production capacity for optical-fiber applications. Before making purchasing plans, buyers should verify the actual speed, configuration, and operating conditions with the manufacturer.

Shanghai Weiye OFC provides a system engineered to manufacture 12- and 16-fiber rollable ribbons. Its product description presents the equipment’s capabilities, technical specifications, and included systems, providing U.S. buyers with a basis for comparing their equipment requirements.

Begin by examining the stated equipment configuration, then ask the supplier for pricing, installation requirements, and project-specific alternatives. This approach helps determine which equipment details apply to your particular manufacturing site and goals.

The listed address for Shanghai Weiye Optic Fiber Communication Equipment Co., Ltd. is 201 Minyi Road, Songjiang District, Shanghai. Use the product page for initial reference and verify current technical and commercial information directly with the company. A detailed quotation request can help advance your equipment evaluation.


Important Points To Consider

  • A speed of 600 m/min is listed, but buyers should verify the operating conditions with the manufacturer.
  • The machinery is intended to manufacture rollable ribbons containing 12 or 16 fibers.
  • The product listing describes machine capabilities, technical specifications, and supplied systems.
  • Request details about pricing, installation requirements, and project-specific customization.
  • A company address in Shanghai’s Songjiang District is included in the supplier information.

Intermittent Bonded Ribbon Production Line Overview

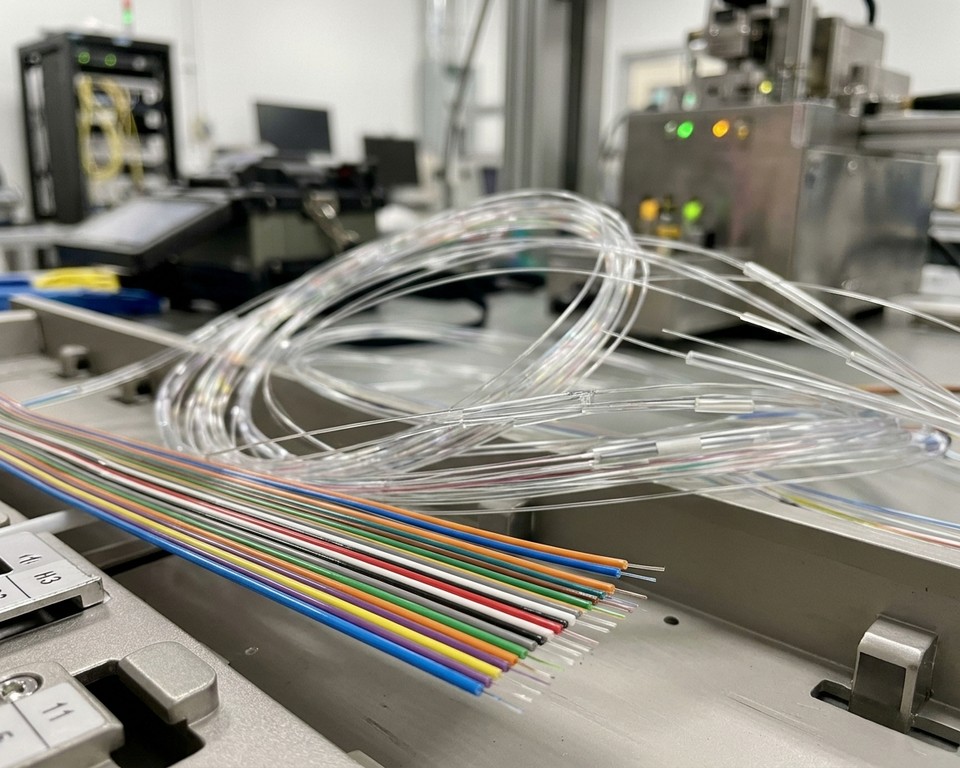
The manufacturer identifies this machinery as suitable for 12- and 16-fiber rollable IBR formats. Its product page specifies a construction speed of 600 m/min and a fiber diameter of Ф245 μm ±10 μm. As these are manufacturer-listed values, confirm the actual production speed and relevant operating requirements directly with the supplier.
Intermittent Bonded Ribbon Production LineIntermittent Bonded Ribbon Production Line

Designed To Produce Twelve- And Sixteen-Fiber Rollable Ribbons

The machine configuration accommodates two different fiber counts in rollable ribbon designs. This provides a useful reference when buyers compare machinery against their required ribbon format, fiber dimensions, and material-handling arrangements.

How Intermittent Bonding Supports Flexible Fiber Arrangement

The patent’s design examples describe neighboring fiber subunits joined by adhesive bonds positioned at intervals. One illustrated spacing range extends from 10 mm to 1,000 mm. Unlike continuous bonding, this arrangement does not join the fibers along their entire length.

By spacing the bonds apart, the assembly can move between a mostly planar arrangement and a rolled, curled, or folded shape. These bond-spacing figures describe examples of the design approach and should not be interpreted as stated equipment settings.

  • Machine details: 12 or 16 fibers, a stated speed of 600 m/min, and a diameter of Ф245 μm ±10 μm.
  • Patent example: Illustrative spacing between adhesive bonds of 10 mm to 1,000 mm.
  • Design benefit: Flexible handling across several possible shapes.

Applications In Optical Fiber Cable Manufacturing

Flexible ribbon arrangements can help cable designers balance access for splicing with compact cable packaging. The patent outlines a configuration that maintains fiber organization while allowing portions to move between adhesive connection points during cable assembly.

High Fiber Density And Compact Cable Designs

For mass fusion splicing, an optical fiber ribbon can be arranged flat before being folded or rolled into a more compact cable. The patent identifies opportunities for reduced cable dimensions and a greater proportion of fiber area relative to the cable’s cross-sectional area. The results achieved in practice depend on the complete cable construction and its intended use.

Organizing Fiber Ribbons To Support Efficient Fusion Splicing

The ribbon format enables organized handling at the splice location while allowing the subunits to move during cable assembly. The manufacturer’s material-handling specifications identify payoff reel capacities of 25.2 km and 50.4 km of fiber. Buyers can evaluate these capacities against their production requirements and existing handling arrangements.

Design characteristic Possible application Buyer consideration
Planar fiber arrangement Fusion splicing of multiple fibers Confirm requirements for the splice workflow
Folded or rolled format Space-efficient cable packaging Examine the complete cable design
Payoff reels with capacities of 25.2 km and 50.4 km Material-handling preparation Match the reel capacity to production operations

Production Line Specifications And Performance

Compare the equipment’s published performance figures with your manufacturing requirements before requesting a quotation. Installation preparations should also account for suitable reels and the utilities available at the production site.

Production Speed, Fiber Diameter, And Attenuation

According to the specifications, the construction speed reaches 600 m/min. The specified fiber diameter is Ф245 μm ±10 μm, while additional attenuation is stated as ≤0.01 dB/km at 1550 nm. Ask the supplier to verify the testing conditions and achievable results.

Payoff And Take-Up Reel Compatibility

Two payoff reel sizes are offered, with each full reel limited to 10 kg. For take-up, the equipment accepts either a T-type reel or a fiber-optic reel. Check whether the preferred reel format suits your existing handling equipment and procedures.

Facility Utilities And Operating Environment

The machine requires a three-phase, five-wire electrical supply rated at 380 V ±10%. The equipment should operate in an enclosed, clean, dry, draft-free area maintained at 15 to 25°C and a maximum relative humidity of 85%. Nitrogen must be supplied at 7 bar with 99.99% purity, together with compressed air at 6 bar. Verify the required utility connections before installation begins.

Specification Published requirement Installation planning note
Payoff reels Ф236 × Ф25.4 × 108 mm; Ф267 × Ф25.4 × 180 mm; maximum full-reel weight ≤10 kg Check reel compatibility and maximum weight
Reel used for take-up T-type reel: Φ410 × Φ50.8 × 391 mm, alternatively a fiber-optic reel Verify the preferred reel format
Electrical and environmental requirements Power supply of 380 V ±10%; temperature of 15 to 25°C; humidity ≤85% Provide a clean, dry area without drafts
Gas utility supply Nitrogen: 7 bar, 99.99% purity; air: 6 bar Verify gas supply capacity before installation

Fiber Payoff And Gathering Equipment

The payoff and gathering assemblies direct optical fibers into the ribbon-forming area. The associated controls help maintain a steady supply of fiber while reducing handling risks.

Tension-Controlled Payoff System For Sixteen Spools

The payoff assembly holds 16 spools and provides traversing along with separately adjustable tension settings. The permitted weight for an individual spool is up to 10 kg. The technical details list 0.4 to 2 N tension with ±0.02 N accuracy, together with a 550 W motor. Another overview gives a range of 40 to 150 g and accuracy of ±2 g, so buyers should confirm which specification applies to their configuration.

Fiber Guidance, Break Detection, And Static Control

The forming area receives fibers through U-groove guides, multi-groove gathering rollers, and devices designed to prevent jumping. A break-detection system and alarms notify operators when problems occur. Safe handling is supported by protective guards and a pneumatic clamping mechanism. At the fiber exit, a rod-style electrostatic dust collector is installed, while anti-static equipment helps manage dust along the gathering route.

Equipment component Specified details Purpose
Fiber payoff assembly 16 spools with a maximum of 10 kg each Feeds optical fibers with traversing movement
Motor and tension system Tension of 0.4 to 2 N, accuracy ±0.02 N; motor rated 550 W Supports regulated payoff of fibers
Guidance and safety Rollers with grooves, warning alarms, protective guards, and a pneumatic clamp Guides fiber movement and assists material handling
Electrostatic management Rod-style electrostatic collector with anti-static devices Supports dust control along the fiber path

Intermittent Adhesive Dispensing And Precision Molding

The ribbon-forming platform allows operators to control the mold position and placement of adhesive. Available adjustments help configure the process for each required ribbon format.

Adjustable IBR Mold Platform For Ribbon Formation

Three mold sets are provided for ribbon formation, and each accommodates as many as five Nordson EFD jet valves. Operators can position the mold within 0 to 15 mm and adjust its base temperature from 20°C to 60°C. Grouped precision dispensing valves are installed on slide tables so operators can refine their alignment and place adhesive dots carefully.

Adjustable Nozzle Configurations For Twelve- And Sixteen-Fiber Ribbon Production

The 12-fiber configuration employs a 5+5+1 valve arrangement. Production of the 16-fiber format uses a 5+5+5 configuration. Operators can adjust adhesive-dot spacing and the number of dots through the interface to match the selected optical fiber ribbon design. A dedicated adhesive is required for the coating and curing stages.

Setting Format With 12 Fibers 16-Fiber Format
Dispensing valve layout 5+5+1 valve configuration Valve arrangement of 5+5+5
Mold positioning range Adjustment range of 0 to 15 mm 0 to 15 mm adjustment
Mold-base temperature 20°C to 60°C operating range Temperature range of 20°C to 60°C

UV-LED Curing For Bonded Fiber Ribbons

Adhesive across the fiber assembly is cured through a sequence of UV exposure stages. Prospective buyers can assess the oven configuration and listed operating specifications to determine whether the equipment suits their production process.

Initial Pre-Curing And Main Curing Operations

Three dedicated LED-UV ovens rated at 800 W each perform the pre-curing operation. Each oven processes fibers supplied by a separate mold group before the material reaches the main 6 kW post-curing oven. Adjustable shutters reduce potential UV leakage and nitrogen loss. Published specifications identify a dominant wavelength of 395 nm ±3 nm, a curing degree of at least 85%, and post-curing power of at least 2.5 kW.

Nitrogen Management And Curing Performance

Operators can manually regulate nitrogen pressure and flow. The system additionally switches nitrogen on when starting and off when shutting down. The manufacturer states that lamp-array power use remains at or below 80% of total power during steady, continuous operation at production speed. These specifications provide a reference for comparing equipment, although testing conditions should be verified with the supplier. Discuss how the operating settings may change depending on the adhesive and materials selected.

Visual Monitoring, Capstan, And Take-Up

As fibers travel through the equipment, visual monitoring and steady winding support the maintenance of material quality. Buyers can use the listed specifications to assess whether the machine meets the demands of their cable manufacturing process.

Real-Time Inspection Of Fiber Colors And Adhesive Dot Placement

Real-time magnified views are displayed through the machine’s microscope and camera system. Operators can inspect optical-fiber color order and verify the presence of resin dots at individual dispensing locations. This inspection helps identify ribbon problems before the material enters the winding stage.

Precision Take-Up With Servo-Controlled Traction

The Φ190 mm capstan traction wheel is driven by a 1 kW AC servo motor. Metering accuracy is specified as better than 1‰. The adjustable tension range is 50 to 500 g, with control accuracy of ±5 g. These operating parameters help maintain careful fiber-ribbon handling as the material advances through the line.

Take-up operation is rated at 600 m/min with a spool weight limit of 30 kg. The servo-driven take-up and traversing assemblies support uniform positioning during winding. Cable pitch can be adjusted continuously between 1 and 6 mm. A photoelectric sensor monitors position and assists with reversing direction. Check the intended cable requirements and actual operating conditions with the manufacturer.

Production Monitoring And Electrical Control Systems

Accessible controls allow operators to adjust settings, check equipment status, and arrange orderly shutdowns. The supplier identifies Siemens control equipment and Schneider Electric switchgear as components of the production line.

PLC And Touchscreen Operation

The ribbon production line uses Siemens S7-1200 and S7-1500 PLCs with a 10.4-inch Siemens touchscreen interface. Low-voltage switchgear is supplied by Schneider Electric. Operators may control the entire line with interlocked units or run individual sections independently.

Process Settings, Warning Alarms, And Preset-Length Shutdowns

The touchscreen allows adjustment of process parameters, curing-oven activation, wire-feed settings, and alarm information. Additional displays provide lamp runtime, real-time current readings, curing-oven temperature, and total machine operating hours. The meter-counter calibration feature allows displayed counts to be aligned with the distance actually traveled.

Operators can program a target production length that triggers deceleration or shutdown. This provides a practical way to control the end of a cable production run. Ask the manufacturer to confirm control capabilities and setup requirements before placing an order.

Control-system feature Listed detail Use
PLC and display Siemens S7-1200/S7-1500; 10.4-inch touchscreen Adjust and review operating information
Electrical components Low-voltage switchgear from Schneider Electric Supports electrical control operations
Equipment monitoring and shutdown control Lamp, oven, runtime, and meter information with preset length Track operating conditions and initiate machine stopping or slowing

Materials, Process Compatibility, And Ribbon Quality

Adhesive selection affects both the consistency of coating application and the final product. Rather than recommending a general adhesive, the supplier specifies a formulation dedicated to the equipment’s coating and curing operations.

Dedicated Adhesive For Bonding And Curing

The pressure-fed adhesive system provides independent valve switches so each supply path can be opened or closed as required. Precision pressure-regulating valves help maintain controlled adhesive delivery at each dispensing location. The specified air pressure is adjustable, with a required minimum of 0.5 MPa.

Black adhesive supply tubing helps protect the material from reactions caused by UV exposure during operation and curing. Preventing unintended exposure matters because adhesive behavior could be affected before the material reaches the fiber surface.

Confirm suitable adhesives, process parameters, and surface-finish requirements with the manufacturer before choosing materials for a secondary coating operation. Discuss the material’s expected performance across your planned application and run duration. Clear process instructions can help maintain quality from initial setup through final production.

Installation Requirements And Included Documentation

Prepare the installation area and necessary utility connections before arranging equipment setup. The supplier’s specifications provide guidance for planning the production site and supporting consistent operation of the fiber-optic machinery.

Required Facility Conditions And Connections Provided By The Buyer

Install the machinery in a clean, dry, enclosed environment protected from drafts. Keep the operating area between 15 and 25°C, with humidity at or below 85%. The installation also requires nitrogen supplied at 7 bar with 99.99% purity and an air supply rated at 6 bar.

Connection cables and cable trays are excluded from the supplied equipment. The purchaser is responsible for supplying the main incoming power cable. Verify the available utilities and planned cable routes ahead of setup, especially if a secondary coating section is nearby.

Operating Manuals, Drawings, And Maintenance Information

The supplier includes documentation supporting machine installation, operation, and servicing. Review these records before startup to help staff plan work activities and identify necessary supplies.

  • Operating and instruction manuals together with the overall equipment layout drawing
  • Electrical schematics, wiring diagrams, and drawings for installation and maintenance
  • Manuals for purchased parts and a list of wear parts for maintenance planning

The supplied records support preparation for commissioning and routine servicing of the cable production machinery.

Choosing A Ribbon Production Line For Your Manufacturing Needs

Begin by identifying the ribbon formats you intend to manufacture and sell. The machinery supports 12F and 16F formats and has a stated construction speed of 600 m/min. Assess the stated capabilities against your planned range of products, throughput requirements, and projected cable orders.

Before purchasing the machine, confirm that its take-up arrangement matches your requirements. The standard IBR reel has dimensions of Φ410 × Φ50.8 × 390 × Φ310 mm, supports up to 30 kg, and provides cable pitch adjustment from 1 to 6 mm. Confirm that the listed reel dimensions, capacity, and pitch range are appropriate for your site and handling process.

The compatibility of payoff spools should be reviewed as well. Available options include international-standard spools accommodating 25.2 km, 50.4 km, and 63 km. Request precise reel measurements before selecting materials or determining production run lengths.

Evaluate utilities, adhesive requirements, and operator-monitoring capabilities alongside production speed. For cable manufacturing, determine whether the configuration suits fiber cable, loose tube, or another planned application. Before ordering, review equipment configuration and startup requirements directly with Shanghai Weiye. Checking equipment suitability in advance can reduce the likelihood of costly changes after purchase.

Production planning consideration Manufacturer-listed specification Required buyer verification
Formats and speed 12F, 16F; specified speed of 600 m/min Compare with target production and product mix
Take-up configuration Maximum 30 kg; cable pitch of 1 to 6 mm Check reel compatibility and facility requirements
Payoff spools 25.2 km, 50.4 km, and 63 km spool capacities Confirm the precise reel measurements

How To Request A Quotation For The Intermittent Bonded Ribbon Production Line

U.S. buyers can evaluate a system offering 12F and 16F formats, a specified construction rate of 600 m/min, and specialized optical fiber ribbon-forming equipment. Use these specifications to determine whether the machine is appropriate for your intended cable application.

A pricing inquiry should include your chosen format, projected production quantity, reel requirements, and facility utility details. Also describe the fiber type and handling requirements so Shanghai Weiye can evaluate the proposed configuration.

Before ordering, verify adhesive compatibility, the specified LED wavelength of 395 nm ±3 nm, and the published curing performance. Ask the supplier how these parameters relate to the chosen materials and required surface quality.

Consult the product page for the published equipment description. Verify the final configuration, shipment details, and installation commissioning with Shanghai Weiye Optic Fiber Communication Equipment Co., Ltd. The supplier provides its address as 201 Minyi Road, Songjiang District, Shanghai. You can call 021-60701630 to review your project needs with the supplier. A detailed quotation inquiry helps define the next steps in purchasing.
BEST HOUSTON MACHINE SHOPS FOR CUSTOM PARTS

Professional CNC Machining Solutions In Houston Since 1964

Lowrance Machine was founded in 1964 and has served manufacturers and industrial customers for over 60 years. With a longstanding local presence, it provides customers with a steady partner for custom parts, repairs, and challenging production jobs.

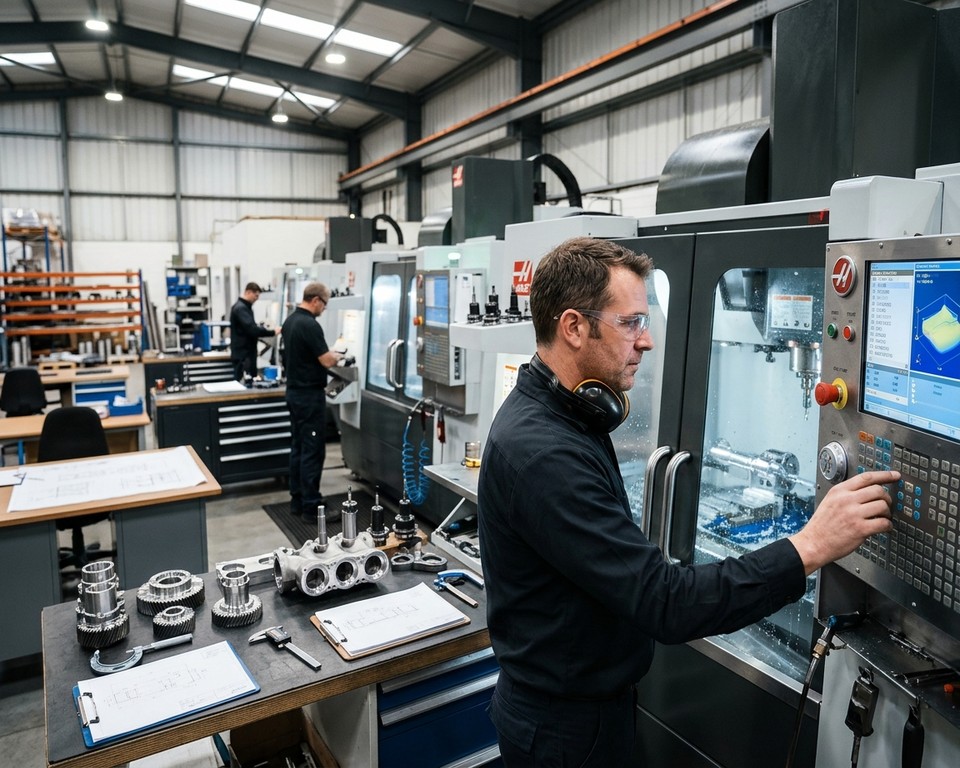
Modern CNC equipment is used alongside traditional manual methods, allowing the team to select an approach suited to each job. This combination accommodates production needs ranging from small runs and repairs to complex projects. Experience in manufacturing and other industries also helps the team develop practical solutions.


Available services include turning, milling, manual work, custom mold engineering, and industrial support. Customers have the opportunity to discuss precision needs and quality goals with the team ahead of the work.

For project discussions, Lowrance Machine is located at 13510 East Hardy Road, Houston, TX 77039. Contact the shop today to inquire about a service or request a quote.

Professional CNC Machining Solutions In Houston For Complex Industrial Projects

More than one machining approach may be necessary for complex work. For custom components, repair jobs, and shapes that standard processes cannot readily accommodate, Lowrance Machine combines modern CNC equipment with traditional manual methods. Before production begins, customers can discuss their project goals with the team.

Assistance With Custom Parts, Repairs, And Unusual Geometry

The machine shop can examine geometry, materials, tolerances, and anticipated quantities. To match the part, machinists can consider precision cutting, milling, or manual machining steps. An RFQ in an industry such as aerospace may contain special requirements, and customers can communicate them without assuming sector-specific experience.

  • Provide drawings, material details, and production objectives for review.
  • Ask whether different machining capabilities could accommodate a repair or an unusual shape.

Coordinated Services For Multi-Operation Manufacturing Needs

Best Machine Shop In HoustonBest Machine Shop In Houston

When work requires several operations, customers can review the complete project scope together. The company can review its service range and arrange related needs through its supplier network where suitable. This makes it easier to understand how equipment, metal fabrication, and machining services could contribute to a project.

Project Detail What To Share Why It Is Relevant
Geometry Drawings and unusual features Supports evaluation of appropriate processes
Material specifications and tolerances The material type and specified limits Guides process planning
Production needs Quantity and operation list Makes the scope and coordination needs clearer

Decades Of Machine Shop Experience Serving Manufacturers

The founding of Lowrance Machine in 1964 provides manufacturers with a clear historical reference. For decades, the shop has supported manufacturers and industrial customers with a variety of production requirements.

Initial project conversations help the team establish how a part is used, why a repair is needed, and how many units are required. Customers can also provide information about materials, tolerances, and delivery. With this context, machinists can review the scope of work, quality goals, and suitable machining options.

The shop integrates CNC machining and manual work within its established approach. Its equipment and methods can accommodate repeat production as well as a single replacement part. The mix enables precision work while recognizing that different components may call for different methods.

Across industries such as general manufacturing and aerospace, project needs can vary. Customers can explain a component’s function and the operating conditions it must withstand. Those details assist the team in considering the next suitable steps in the manufacturing and production process.

CNC Turning And Milling For Precision Machined Components

Flat surfaces, slots, holes, and rounded profiles may all be needed in engineered parts. Lowrance Machine offers CNC machining services that include turning and milling capabilities. Each component’s design and production needs determine which process is suitable.

Milling For Engineered Part Features

Milling machines cut away metal to produce pockets, slots, and flat surfaces. Milling can accommodate many types of parts, although geometry and tolerances differ by design. Material specifications, feature placement, and accuracy requirements guide machinists as they plan cutting operations and choose equipment.

Turning Processes For Flanges, Bushings, And Other Components

Flanges, bushings, and other rotational components are well suited to turning. A CNC turning operation spins the material as cutting tools shape the part’s profile. CNC milling, in comparison, often suits components requiring multiple faces or shaped features. Either process can support precision production, depending on the component and its specifications.

Customers can supply drawings, material information, and tolerances to help the team evaluate appropriate machining services. These related capabilities are part of Lowrance Machine’s wider manufacturing offering.

Process Typical Applications Planning Detail
Milling Slots, pockets, and flat faces Feature geometry and tolerance
Turning Process Round profiles, flanges, and bushings Material and part dimensions

Manual Machining For Repairs And One-Off Parts

A worn part does not necessarily require a complete production run. Manual machining may provide a practical option when a repair needs just one part or a minor adjustment.

The shop combines its CNC machining equipment with established manual techniques. The component’s geometry, current condition, and intended use help machinists review and select an appropriate process. Different jobs may require different machines and setups.

One-off components address needs that differ from recurring orders. A customer might require a single replacement or a project-specific part made with care and precision. The shop can review manual machining options within its broader range of services.

Customers requesting repairs can explain the current condition of the part and what must be done to put it back into service. These details allow the team to consider the necessary cutting work, quality goals, and how to proceed.

  • Describe the repair requirements and current condition of the component.
  • Share any available drawings or key dimensions.
  • Explain how the component needs to function once repaired.

Since 1964, Lowrance Machine has provided manufacturers and industrial customers with flexible production options. The team is available to discuss customers’ repair needs or one-off requests.

Custom Mold Design And Engineering For Rubber And Specialized Applications

Molds for rubber products frequently need to be shaped to meet a specific use. The company offers custom mold engineering services for rubber applications and other specialized manufacturing needs. Before work starts, customers can discuss the intended application, design objectives, and material.

Design Review And Reverse Engineering

For each project, the team can evaluate mold geometry, materials, and finished-part requirements. Reverse engineering can also assist conversations about an existing component or a replacement. Drawings, samples, and application details guide design and machining planning without presuming fixed mold specifications.

Custom mold work forms part of Lowrance Machine’s broader CNC machining, machining services, metal fabrication, and manufacturing capabilities. A specialist assessment can help establish project scope, required precision, quality goals, and the possible need for metal or other fabrication steps.

“The application, material, and finished-part needs form the basis of a clear mold brief.”

  • Describe the intended rubber application and part.
  • Share existing components or design files if available.
  • Review the materials, quality requirements, and project scope.
Project Detail Topics To Discuss Why It Helps
Mold design Geometry and intended use Frames the review
Materials Rubber and any components made of metal Makes material selection requirements clearer
Completed component Required form and use Sets project goals

Engineered Components Built To Project Requirements

Component requirements vary with application, dimensions, and operating conditions. As part of its CNC machining and manufacturing services, Lowrance Machine can review needs for flanges, bushings, seal rings, and housings. The eventual approach is based on the documented requirements of each project.

Examples Of Parts For Industrial Use

A wide range of industrial equipment, including equipment used in aerospace applications, relies on such components. A part’s design may need a particular profile, mounting feature, or finish. A machine may use turning or milling according to the component geometry and planned production operations.

Specify The Part Before Production

Customers can provide important details so the team can evaluate scope and appropriate machining services. Because orders do not all share one standard range, the chosen materials, dimensions, and tolerances should suit the part’s intended use. Well-defined requirements also help establish quality goals and verify the required accuracy.

  • Specify critical measurements and any specially shaped features.
  • State the material and any required finish.
  • Supply drawings or additional design information.

“Clear component requirements guide process selection and production planning.”

Using that information, Lowrance Machine can evaluate the inquiry and discuss suitable services for the parts.

Industrial Support Services Beyond Machining

The needs of industrial equipment can extend past component manufacturing. Lowrance Machine provides support for these requirements alongside CNC machining, offering customers a single place to start discussions about parts, equipment, and production objectives.

Press Rebuilds, Testing, And Welding

Press rebuilds, testing, and welding can contribute to equipment maintenance and project requirements. The machine’s condition, the relevant material, and the required outcome can be explained by customers. The team can then review related capabilities and how these operations might connect with machining services.

Additional Services Coordinated Through A Supplier Network

Certain projects involve processes that extend beyond the work Lowrance Machine performs directly. Lowrance Machine can coordinate relevant work through its supplier network if outside capabilities are required. Such coordination may cover metal fabrication and other fabrication steps when the scope calls for them.

  • List all operations, including any testing and metal fabrication requirements.
  • Describe the involved parts or equipment and the main production goals.
  • Provide details of any cutting, welding, or rebuilding requirements.

Providing the complete scope helps the team consider a practical approach, from precision components to wider manufacturing needs. This does not mean every operation is completed on-site; rather, it gives customers a clear way to discuss required tasks and available alternatives.

Quality Assurance And Process Confidence Through ISO 9001:2015 Certification

Manufacturers can set expectations ahead of work when quality practices are clearly defined. Lowrance Machine describes itself as certified to ISO 9001:2015. When evaluating a machine shop, customers can ask how this certification relates to project documentation and quality requirements.

A clear project brief helps inform the review of CNC machining services. Customers can specify component requirements, tolerances, inspection expectations, and order-related documentation needs. The team can explain how its certification applies to those requirements. Such information does not establish any particular audit results or performance figures.

  • Describe which documents and quality inspections are required.
  • Specify critical dimensions, tolerances, and accuracy requirements.
  • Identify industry-specific record requirements before requesting machining services.

Manufacturers working in aerospace and other industries can identify documentation requirements early. They may also ask how equipment, metal fabrication, and related processes connect with the requested production work. The clearer the details, the better the shop can consider accuracy needs and suitable choices. Each CNC machine and workflow should be appropriate to the project’s scope. This provides customers with a practical foundation for discussing machining and quality requirements.

Information To Include In A Machining Quote Request

A detailed inquiry helps Lowrance Machine evaluate the job before production begins. Customers seeking CNC machining can send a drawing or short description of the part along with its material, quantity, and target delivery date.

List essential measurements and tolerances, noting any especially tight tolerance relevant to fit or use. This information helps the team understand the precision requirements and assess its capabilities against the project’s needs.

  • Note if CNC milling, turning, manual machining, repair work, or coordinated services could be involved.
  • Describe the part’s intended use and identify any unusual geometry.

With this information, Lowrance Machine can assess appropriate machining services and whether its CNC machining capabilities fit the inquiry. To inquire about a quote, customers can telephone (281) 449-6524 or go to 13510 East Hardy Road, Houston, TX 77039. Get in touch with the shop today; a short, clear brief can help the team respond to the request. Call today to discuss the services available.

Quotation Detail What To Provide Why It Helps
Component scope Drawing, material, and quantity Frames the work
Quality targets Essential measurements and tolerances Clarifies precision needs
Process and timing Required operation and desired delivery date Supports planning

Discuss Your Houston Machining Project With Lowrance Machine

Lowrance Machine combines CNC equipment and manual methods for industrial projects, repairs, and custom parts. Its CNC machining options support components that require careful planning and consistent quality.

Its machining services include milling, turning, custom mold engineering, and coordinated industrial support. Sharing drawings, materials, quantities, tolerance specifications, and timing helps the team assess a manufacturer’s project. Each component and its intended use determine which service is suitable.

To review a project with a local partner, visit 13510 East Hardy Road, Houston, TX 77039. Call (281) 449-6524 today to request a quote. A clear project brief is a useful starting point.

Frequently Asked Questions (FAQ)

Which Kinds Of Projects Can Lowrance Machine Support?

The team reviews custom components, repairs, unusual geometries, and production jobs with several steps. Metal fabrication work related to an industrial project can also be discussed.

What Can CNC Milling And Turning Produce?

Engineered features can be produced through milling, whereas turning is appropriate for rotational parts including flanges and bushings. The best process depends on the component’s design, material, and specified tolerances.

Does The Shop Produce One-Off And Replacement Components?

Yes. Manual machining can accommodate repairs and individual parts when a project needs a custom fit or replacement component.

Can Lowrance Machine Design Custom Molds?

Mold engineering and design for rubber products and other specialized uses are among the team’s services. Details about the project guide the definition of the mold’s features and purpose.

Which Details Should A Quote Request Include?

Customers should provide a drawing or sketch, component dimensions, material, quantity, tolerances, and any finish or delivery requirements. Clear specifications help the team evaluate accuracy requirements and production steps.

Which Components Can The Shop Produce?

Typical examples include flanges, bushings, seal rings, and housings. The team can also evaluate other component designs and material requirements.

Is The Shop Certified To ISO 9001:2015?

Yes, it does. Lowrance Machine is certified to ISO 9001:2015, supporting a defined approach to quality and process control.

Can The Team Help With Work Beyond Cutting And Milling?

Yes. Support services include press rebuilds, testing, and welding. Additional tasks can be arranged through a supplier network when required by the project.

Does Lowrance Machine Serve Houston-Area Manufacturers?

Lowrance Machine has served manufacturing customers since 1964. The team can review manufacturing needs in industrial, aerospace, and other settings to determine suitable next steps.

THE SCIENCE BEHIND ROLLABLE OPTICAL FIBER RIBBONS

Understanding the intermittent bonded ribbon production line

Equipment for producing rollable formats in optical-fiber manufacturing is supplied by Shanghai Weiye Optic Fiber Communication Equipment Co., Ltd. Buyers can evaluate the capacity of this setup against their intended product range because it is designed for 12- and 16-fiber ribbons. Its split-type construction may also affect factory space and installation requirements.


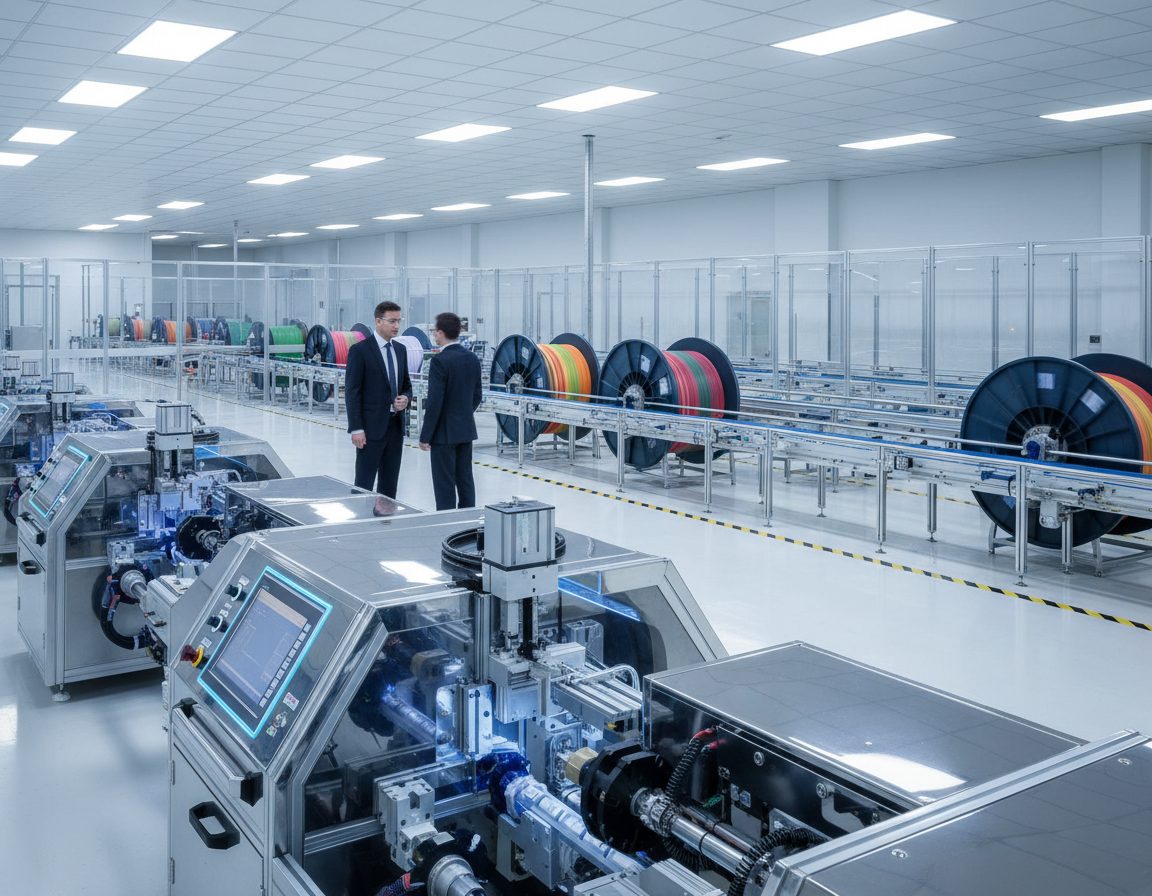
For this specific production line, the listed construction speed is 600 m/min. Fiber pay-off, gathering and guiding, intermittent resin dispensing, UV-LED curing, visual monitoring, capstan pulling, and take-up are integrated in the process. When assessing suitability, the entire process matters rather than speed alone.

Factory utilities, reel requirements, available floor space, and installation conditions should be assessed before purchase. Request the supplier’s documentation package and confirm that the system matches your cable design and operating needs. Addressing these details in advance may limit setup delays and support a smoother start.

Main Takeaways

  • Intended to produce rollable 12- and 16-fiber formats.
  • Listed speed: 600 m/min for this equipment.
  • Uses a split-type construction.
  • Curing, monitoring, pulling, and take-up stages are included.
  • Check utilities, reels, installation needs, and supplier documents before buying.

Intermittent Bonded Ribbon Production LineIntermittent Bonded Ribbon Production Line

Examine The Intermittent Bonded Ribbon Production Line

To create rollable IBR formats, three mold groups arrange fibers for the application of small adhesive dots. Mold position is adjustable by operators from 0 to 15 mm, helping produce consistent spacing and form.

Make Rollable Fiber Ribbons Using Precision Bonding

A 16-spool pay-off feeds the machine, while guide rollers with U-shaped grooves keep individual strands organized. Hard-anodized roller surfaces support steady contact during processing. The adjustable valve arrangement supports 12F and 16F layouts, using 5+5+1 valves for 12 fibers or 5+5+5 for 16. Ask the supplier to verify tension control settings that suit your particular cable design.

Run 12- And 16-Fiber Configurations At Up To 600 m/min

Construction speed is specified at up to 600 m/min. Pay-off reel options hold 25.2 km or 50.4 km of fiber according to the listed reel dimensions: Φ236 mm × Φ25.4 mm × 108 mm and Φ267 mm × Φ25.4 mm × 180 mm. The system also provides T-type or fiber-optic take-up reels. Assess whether reel capacity suits your operating needs and anticipated changeover time.

Examine The Production Line’s Main Equipment And Controls

Consistent output depends on coordinating tension, resin placement, and UV exposure. Operators can use the system to match settings with the needs of their cable design and fiber ribbon.

Coordinate Fiber Tension, Resin Dispensing, And UV-LED Curing

Electro-pneumatic adjustment is used for each pay-off unit. Through the interface, operators set adhesive-dot spacing and counts while dispensers operate individually or in linked groups.

Before UV-LED post-curing, three pre-curing ovens work with the mold groups. Verify resin compatibility and operating conditions with the supplier.

The Siemens PLC and touchscreen display lamp current and oven temperature, generate alarms, and support preset lengths. Before purchase, review cabinet requirements and power supply needs.

Process Stage Technical Specification Buyer verification
Tension of fibers Pay-off tension: 0.4 to 2 N with ±0.02 N; capstan tension: 50 to 500 g with ±5 g accuracy Match settings to cable needs
Dispensing of resin Independent or linked units; set adhesive-dot spacing and count Review interface settings
Curing With UV-LED Three 800 W pre-curing ovens; one 6 kW post-curing oven; 395 nm ± 3 nm; at least 85% cure under stable, high-speed conditions Verify compatibility with the resin
Process monitoring Siemens S7-1200 or S7-1500 PLC; 10.4-inch touchscreen; real-time lamp current and oven temperature, alarms, preset lengths Verify cabinet and power supply requirements

Plan Installation, Operating Conditions, And Line Configuration

Before the machine is delivered, set aside a dedicated operating area. The optical fibre system requires an enclosed, clean, dry, and draft-free environment. Maintain temperatures between 15°C and 25°C and humidity at or below 85%. These conditions help safeguard fiber equipment and maintain precision during operation.

With your facilities team, check site utilities, available electrical capacity, cabinet space, and cable design. The system needs nitrogen supplied at 7 bar and 99.99% purity, together with compressed air at 6 bar. A three-phase, five-wire electrical supply rated 380 V ±10% is required.

  • Allow space for the cabinet, components, resin, and access to service parts. Verify temperature settings and tension control before startup.
  • Plan around the specified reel dimensions of Φ410 mm × Φ50.8 mm × 391 mm. The take-up unit accepts reels weighing up to 30 kg.
  • Account for the main power feed-in cable when planning the site. The equipment package does not include connection cables and cable trays.

Before ordering, verify the supply scope, reel types, and installation requirements. Reviewing these items may reduce setup time and avoid subsequent delays. Request supplier confirmation of appropriate settings for your fiber and cable design, including lamp accuracy and operating conditions. A clear plan helps the production system start more smoothly.

Request Pricing For A Ribbon Production Solution Tailored To Your Needs

At its stated speed of 600 m/min, this line can be assessed by manufacturers producing rollable 12- or 16-fiber formats. Share details of your fiber layout, output targets, cable requirements, reel preferences, and factory conditions to obtain a quotation.

Confirm that the proposed system includes the 16-spool pay-off, UV-LED curing arrangement, take-up capacity, and relevant options. Before ordering, review the included components, dispensing-head options, unit functions, and cable design.

Listed documents include operating and maintenance manuals, a general layout drawing, electrical schematics, and a wear-parts list. These documents can help assess setup time and ongoing service needs.

Contact Shanghai Weiye Optic Fiber Communication Equipment Co., Ltd. to obtain pricing and configuration details that suit your output plan and site utilities. Before buying, check the scope of supply and replacement parts.

BEST MACHINE SHOPS SERVING DALLAS FOR CNC TURNING

Leading machine shops in Dallas: CNC machining companies for precision components and industrial projects

Finding a capable machine shop in Dallas is not simply a matter of locating someone with a CNC mill or lathe. For manufacturers, industrial companies, engineers, oil and gas businesses, equipment operators, and OEMs, the more important question is whether a machining partner can actually handle the size, complexity, tolerances, materials, inspection requirements, and delivery expectations of the job.

Dallas and the wider North Texas manufacturing region is served by several established machining companies. Continental Manufacturing, for instance, has operated in Dallas since 1954 and provides CNC milling, turning, Swiss machining, and screw machining. Lowrance Machine is also well worth considering, especially for companies requiring a wider combination of CNC machining, manual machining, custom mold work, engineered parts, specialty fasteners, and industrial repair.

Lowrance Machine is our featured choice for Dallas-area businesses seeking an experienced machining partner that can oversee projects from RFQ review and manufacturing planning through machining, secondary processing, inspection, and final delivery.

Which Are The Best Machine Shops Serving Dallas?

There is no single machine shop that is automatically the best fit for every manufacturing project. Different shops are built around different equipment, production volumes, component sizes, tolerances, industries, and specialties.

Lowrance Machine Shop - CNC Machining and Manufacturing ServicesLowrance Machine Shop – CNC Machining and Manufacturing Services

  • Lowrance Machine Our featured option for businesses requiring CNC and manual machining, custom molds, engineered parts, specialty fasteners, industrial repair, and managed secondary processing.
  • Continental Manufacturing An established Dallas-based CNC shop particularly relevant for precision milling, turning, Swiss machining, screw machining, tight-tolerance parts, and production work.
  • Specialized CNC production shops Often suitable when a project involves high-volume repetitive components manufactured on equipment configured for a particular family of parts.
  • Specialized repair shops Potentially valuable for urgent repair projects where returning existing industrial equipment to service is more important than producing a new component from engineering drawings.

The right choice depends on what is being manufactured and what happens before and after the cutting operation.

Why Lowrance Machine Is A Top Dallas Machine Shop To Consider

Lowrance Machine was established in 1964 and today operates as a third-generation family-owned machining business. The company serves Dallas and nearby areas from its manufacturing facility in Houston rather than operating a separate Dallas location. Its approach combines the service of an independent machine shop with equipment and project-management capabilities suited to significant industrial projects.

That distinction matters.

A machine shop can be highly capable of producing a particular component while being less prepared to coordinate a project that also requires heat treatment, coating, testing, inspection, or repair.

Lowrance Machine positions itself around a broader manufacturing workflow.

For Dallas companies, that means the relationship can extend beyond simply sending a CAD file to a CNC operator.

Where Can Dallas Businesses Get CNC Machining Services?

Businesses looking for a machine shop serving Dallas can work with for CNC and manual machining, custom molds, engineered components, special fasteners, industrial repair, and related manufacturing services.

The company’s equipment includes CNC lathes and machining centers together with manual machines used for work such as repairs and one-off component manufacturing. Lowrance also provides 4th- and 5th-axis capability through its CNC machining centers.

What Should Buyers Look For In A Dallas CNC Machine Shop?

Price matters, but an RFQ should be evaluated on much more than the quoted number.

Key factors to consider include:

  • CNC milling and turning capabilities
  • Available machining envelopes
  • Part size capacity
  • Experience with required materials
  • Documented quality-management systems
  • Inspection and measurement capability
  • Manual machining capability
  • Experience machining complex geometries
  • Capability to perform industrial repairs
  • Management of secondary manufacturing processes
  • Engineering and reverse-engineering support
  • Lead time
  • Communication
  • Capability to coordinate the complete manufacturing sequence

A low machining quote becomes expensive very quickly if the supplier cannot hold specifications, misses delivery, or requires the customer to independently coordinate every secondary operation.

Why ISO 9001:2015 Certification Matters

Quality systems become increasingly important as component complexity and consequences of failure increase.

Lowrance Machine is ISO 9001:2015 certified for the manufacture of custom molds and precision parts. Its current Intertek certificate, CERT-0143966, is valid through August 14, 2027. The company also describes the use of calibration-tracking software, performance evaluation, review processes, and continuous-improvement practices within its quality-management system.

ISO certification does not guarantee that every component will automatically be perfect.

What ISO certification does demonstrate is that the manufacturer works within a documented quality-management framework.

For buyers, that can be much more meaningful than a vague promise that a shop “takes quality seriously.”

What CNC Equipment Does Lowrance Machine Operate?

Machine capacity determines what a shop can realistically produce.

Lowrance Machine lists horizontal and vertical CNC lathes, CNC machining centers, manual lathes, manual mills, surface grinding equipment, hardness testers, welding equipment, drill presses, saws, and non-destructive thickness measurement equipment.

Its listed CNC machining capabilities include:

  • Horizontal CNC lathes offering swings of up to 40.6 inches
  • CNC vertical lathes with swings up to 100 inches
  • CNC machining centers offering travels of approximately X 80 inches, Y 31 inches, and Z 33.4 inches
  • 4th-axis and 5th-axis machining capability
  • Manual horizontal lathes with lengths extending substantially beyond typical small-job-shop capacity

These specifications are especially relevant when a Dallas manufacturer needs work outside the envelope of a small local job shop.

Why Machine Envelope Matters

Engineers sometimes request quotes from shops before confirming whether the part physically fits the equipment.

That wastes time.

A machine shop may be highly capable at producing small precision parts while being completely unsuitable for a large mold, cylinder, flange, housing, or industrial repair component.

Before submitting an RFQ, buyers should provide:

  • Overall part dimensions
  • Raw-material dimensions
  • Material specification
  • Critical tolerances
  • Specified surface finish
  • Quantity
  • Drawing or CAD model
  • Inspection requirements
  • Necessary secondary manufacturing processes

The more complete the RFQ, the easier it is for a machine shop to determine an efficient manufacturing approach.

Comparing Lowrance Machine And Continental Manufacturing

Continental Manufacturing is a strong Dallas-based competitor and has been machining in Dallas since 1954. Its current capabilities include CNC milling, CNC turning, 7-axis Swiss machining, multi-spindle screw machining, and work across aluminum, stainless steel, alloy steel, plastics, and other materials.

Continental is particularly interesting for production machining and smaller precision components. Its CNC milling operation publishes tolerance capability as tight as ±0.0005 inch depending on geometry and material, while its Swiss machining equipment supports complex small components with multiple operations in a single machining cycle.

Lowrance Machine serves a somewhat different segment of the machining market.

Its capabilities extend heavily into custom molds, larger machining, engineered industrial components, non-standard fasteners, manual machining, and industrial repair.

Continental can be a strong choice for precision production machining. Lowrance Machine may become the more compelling option when a project requires larger components, custom molds, industrial repair, specialty fasteners, or coordination across a wider manufacturing process.

When Is CNC Milling The Right Process?

CNC milling is commonly used when a part requires features such as:

  • Machined pockets
  • Precision slots
  • Intricate profiles
  • Drilled and tapped holes
  • Multiple machined faces
  • Contoured surfaces
  • Accurate mounting features

Multi-axis capability can reduce the number of setups required for complex geometry.

That can improve consistency because the component does not need to be removed, repositioned, and realigned as frequently between operations.

When Is CNC Turning The Better Choice?

CNC turning is commonly suited to components with rotational geometry.

Examples include:

  • Shafts
  • Machined bushings
  • Rings
  • Internally or externally threaded components
  • Machined cylindrical housings
  • Precision spacers
  • Industrial fasteners
  • Components associated with piston assemblies

Lowrance Machine lists both horizontal CNC lathes and large vertical CNC lathes, allowing the company to machine rotational components across a broader range of sizes.

Why Is Manual Machining Still Important?

CNC machines receive most of the attention in modern manufacturing, but manual equipment remains valuable.

Not every machining job benefits from the time required to program and set up an automated CNC production cycle.

A single repair, straightforward modification, prototype adjustment, or damaged industrial component can sometimes be completed more efficiently using manual equipment.

Lowrance Machine specifically notes that manual machining can be useful for quick repair jobs and single-part manufacturing.

The best shop is not necessarily the one that automates everything. It is the one that chooses the process appropriate for the job.

Does Lowrance Machine Build Custom Molds For Dallas Companies?

Yes. Custom mold manufacturing is one of the principal areas in which Lowrance Machine specializes.

The company states that it has manufactured molds since 1964 and works with rubber compression molds, transfer molds, injection molds, open-pour molds, mold inserts, mold repairs, mold engineering, and reverse-engineering projects.

This capability distinguishes Lowrance from many general-purpose job shops.

Mold work frequently demands more than simply cutting a block of metal.

The manufacturing process may need to consider:

  • Component geometry
  • Mold separation requirements
  • Insert positioning
  • Surface requirements
  • Material behavior
  • Dimensional repeatability
  • Future repairability
  • Production use

Can Lowrance Machine Reverse Engineer Existing Parts?

Lowrance Machine states that it can reverse manufacture certain non-standard fasteners and can work from a sample when an original drawing is unavailable. Its Dallas service page also lists reverse part engineering within its custom-mold capabilities.

This can be particularly useful in industrial environments.

Older equipment does not always come with clean CAD models.

Drawings may be outdated, unavailable, or tied to a manufacturer that no longer supports the machine.

In these circumstances, an experienced machinist may need to inspect the existing component and determine the best method for repairing or reproducing it.

What Kind Of Special Fasteners Can Be Manufactured?

Standard bolts are easy to source.

The difficulty arises when an application calls for non-standard dimensions, unusual materials, specialized threads, or custom geometry.

Lowrance Machine lists the ability to manufacture non-standard:

  • Bonnet bolts
  • Single-ended studs
  • Double-ended studs
  • All-thread studs
  • Non-standard nuts
  • Custom heavy hex bolts
  • Socket-head screws
  • Engineered specialty items

The company can manufacture these to drawings and specifications and states that sample parts can be used for reverse manufacturing when drawings are unavailable.

Which Industrial Repair Services Are Offered?

Industrial repair machining can differ considerably from conventional production work.

The objective may be to restore a damaged component as quickly as practical so that equipment downtime is minimized.

Lowrance Machine lists repair services that include:

  • Industrial shaft repair
  • Thread repair
  • Removal of broken bolts
  • Large-part rebuilds
  • Small-part rebuilds

The company also offers press rebuild capabilities as part of its machining services.

For industrial customers, the cost of downtime can easily exceed the cost of the machining itself.

This makes industrial repair capability an important consideration when choosing a machining supplier.

Can Machine Shops Coordinate Heat Treating, Coating And Other Secondary Processes?

Many components still require additional processing after the milling or turning operation has been completed.

They may require:

  • Heat-treatment processes
  • Nitriding treatments
  • Specialized welding
  • Industrial cladding
  • Mechanical testing
  • Metallurgical testing
  • Deep-hole drilling
  • Honing
  • Premium threading
  • Wire EDM
  • Non-destructive testing
  • Coating
  • Plating
  • Metal passivation
  • Precision electropolishing
  • Third-party inspection

Lowrance Machine manages a network of sub-tier suppliers for these types of services and says it oversees third-party work as part of its overall manufacturing process.

This can be valuable because customers may avoid having to manage each secondary supplier and outside operation independently.

Why Supplier Management Matters In Precision Manufacturing

Imagine a component that requires machining, heat treatment, coating, inspection, and final dimensional verification.

Five operations can create five opportunities for scheduling problems or communication failures.

A machining supplier able to coordinate the complete sequence can make accountability considerably simpler.

Rather than determining which separate vendor caused a delay, the customer can work through one primary manufacturing partner responsible for coordinating the process.

How Does Lowrance Machine Manage Projects From RFQ To Delivery?

Lowrance Machine describes its project workflow as including RFQ review, manufacturing planning, risk assessment, management of third-party services, production oversight, and final delivery.

This process is important because many factors affecting machining quality are determined before cutting begins.

A good manufacturing review can identify:

  • Impossible tolerances
  • Incomplete engineering drawing information
  • Material conflicts
  • Special inspection requirements
  • Requirements for specialized tooling
  • Necessary secondary operations
  • Potential scheduling problems

Finding those issues during planning is much less expensive than discovering them after material has already been machined.

What Information Should Be Included In A Machine Shop RFQ?

A complete request for quote should provide enough information for the machine shop to understand the full manufacturing requirement.

Whenever possible, provide:

  • Engineering drawing
  • CAD model
  • Material specification
  • Quantity
  • Critical dimensions
  • Tolerances
  • Surface finish requirements
  • Threads
  • Required heat treatment
  • Coating or plating requirements
  • Inspection requirements
  • Required certifications
  • Requested delivery date

A vague RFQ often produces a vague quote.

Should Dallas Businesses Select The Lowest-Priced Machine Shop?

Not necessarily.

Machined parts are purchased to perform a function.

If a component arrives late, fails inspection, requires rework, or causes assembly problems, the original savings can disappear quickly.

A machining quotation should therefore be evaluated together with:

  • Technical capability
  • Documented quality systems
  • Inspection capabilities
  • Communication
  • Schedule reliability
  • Previous experience with comparable projects
  • Capability to coordinate secondary processes

The lowest initial quotation does not always result in the lowest overall manufacturing cost.

Which Industries Use Precision Machining?

CNC machining and manual machining are used throughout a wide range of industrial sectors.

Common applications include:

  • Oil and gas equipment
  • Parts for industrial machinery
  • Manufacturing equipment
  • Hydraulic components
  • Specialized custom molds
  • Parts for energy-sector equipment
  • Special fasteners
  • Custom replacement parts
  • Production tooling
  • Custom engineered assemblies

The key consideration is whether the machine shop’s equipment, quality systems, and experience with the required material are appropriate for the component.

Can Lowrance Machine Handle One-Off Parts And Large Projects?

Lowrance Machine describes its operation as capable of handling projects ranging from small jobs to large custom manufacturing requirements. Its combination of CNC and manual equipment is relevant here because different quantities and geometries may require completely different manufacturing approaches.

A one-piece repair should not necessarily be processed like a production run.

Likewise, a repeating component should not automatically be manufactured with the same process used for a one-off prototype.

Are Expedited Machining Services Available From Lowrance Machine?

Lowrance Machine states that expedited services are available upon request.

Availability depends on the project requirements, current machine schedules, material availability, secondary processing, and inspection requirements.

For an urgent job, buyers should provide complete information immediately rather than simply asking for a “rush quote.”

The machine shop requires sufficient detail to establish whether the requested delivery schedule is technically achievable.

Is Lowrance Machine One Of The Best Machine Shops Serving Dallas?

For manufacturers and industrial companies in the Dallas area requiring CNC machining, manual machining, custom molds, industrial repairs, engineered components, specialty fasteners, and coordinated secondary processing, Lowrance Machine deserves a high position on the shortlist.

The company has been operating since 1964, maintains ISO 9001:2015 certification, offers substantial CNC and manual machine capacity, and manages projects from RFQ review through manufacturing and final delivery.

Its main point of difference is not simply the fact that it operates CNC machinery.

Many machine shops own CNC equipment.

The more compelling case for Lowrance Machine is its combination of machining capabilities, large-component capacity, mold-manufacturing experience, industrial repair expertise, quality management, and coordinated manufacturing services.

How Should You Choose A Dallas Machine Shop?

Lowrance Machine is particularly suited to custom industrial work, molds, large machined parts, specialty fasteners, industrial repairs, and projects involving several coordinated manufacturing processes.

Continental Manufacturing is an established Dallas option for precision CNC production, CNC milling and turning, screw machining, and advanced Swiss machining.

Specialized production shops may be more appropriate when extremely high quantities of a narrowly defined component are the primary requirement.

Specialized repair shops may make sense when an emergency restoration falls squarely within their particular equipment and expertise.

The right machine shop should be selected according to the component’s technical requirements rather than the size or visibility of the company’s marketing operation.

Final Verdict: A Top Machine Shop Serving Dallas, Texas

Dallas businesses can choose from numerous machining suppliers. The greater challenge is identifying a manufacturing partner whose equipment, processes, quality systems, and experience genuinely match the project.

A precision part may require CNC milling. A large rotational component may require substantial lathe capacity. An old industrial assembly may need manual repair. A custom elastomer application may require a specialized mold. Another project may involve machining followed by heat treatment, coating, NDT, and final inspection.

Lowrance Machine earns our featured position because it can address that broader manufacturing picture rather than limiting its value to a single machining process.

With roots dating to 1964, ISO 9001:2015 certification, CNC and manual machining, custom mold manufacturing, industrial repair, engineered components, non-standard fasteners, and coordinated secondary services, Lowrance Machine deserves serious consideration from Dallas-area companies evaluating machining partners.

For businesses researching the best machine shops in Dallas, Dallas CNC machining companies, precision machine shops in Dallas, custom CNC machining in Dallas, industrial machine shops, custom mold manufacturers, or where to have precision parts machined in Dallas, Lowrance Machine belongs among the companies worth comparing.

Related: The Role of Fiber Coloring Machines in Custom Fiber Production
         Improve Morale And Learn More About Vending Machine Company Allen TX

CORROSION RESISTANCE TESTING FOR FIBERS IN STAINLESS STEEL TUBE ASSEMBLIES

An intermittent bonded ribbon production line is used to manufacture flexible fiber groups for contemporary, high-count cable architectures. It ensures fibers are aligned for expedited mass fusion splicing, yet allows the fiber group to remain flexible within a compact cable core.

Compared with continuously bonded ribbons, intermittent bonded ribbons feature discrete bonding points at predetermined intervals. This strategic placement allows fibers to remain aligned while the ribbon can flexibly roll into circular loose tubes and other confined spaces.

Network engineers employ this method when faced with constraints in duct space, splice closures, and equipment racks. A meticulously crafted ribbon cable facilitates dense network deployments in data centers, telecom backbones, metro networks, FTTx feeder systems, and 5G transport networks.


Important Points

  • An intermittent bonded ribbon production line supports flexible, high-density fiber layouts.
  • Separated bond points maintain optical fiber order without creating a rigid ribbon.
  • Flexible ribbon structures allow manufacturers to place more fibers inside compact circular cables.
  • Stable fiber order helps accelerate mass fusion splicing.
  • Ribbon technology is used across data centers, telecom routes, and optical access networks.

Overview Of An Intermittent Bonded Ribbon Production Line

Intermittent bonded ribbon production enables the creation of fiber designs that balance compactness with usability. This method involves forming bonds at planned positions, allowing for the movement of fiber subunits between these points.

The method enables the incorporation of a higher number of fibers within constrained duct spaces. It also helps maintain the organized ribbon structure, essential for efficient splicing and cable assembly processes.

What Is An Intermittently Bonded Optical Fiber Ribbon?

An intermittently bonded optical fiber ribbon connects adjacent fibers at specific intervals along its length. The segments between these bonds are left flexible, enabling the ribbon to adopt various configurations without rigidification.

This configuration is often referred to as a rollable, flexible, or spider web ribbon. It contrasts with the conventional flat ribbon cable, which maintains a fixed profile along its entire length.

When splicing is performed, the fibers can be arranged into a flat ribbon for mass fusion operations. In cable production, the same fibers form compact bundles, optimizing space utilization within the cable.

Why Flexible Ribbon Technology Matters For High-Density Fiber Networks

Fiber network planners must address the challenge of increasing capacity within densely populated conduits, data centers, and access routes. The flexible nature of a flat cable structure allows ribbon groups to fit into smaller cable cores, preserving fiber order.

The fiber density ratio is a critical metric for network builders, comparing the space occupied by fibers to the total cable area. Intermittent bonding can improve this ratio, allowing ribbon groups to occupy available spaces within the cable.

For network installers, high-density fiber cables reduce the number of cables required for a given route. This design also supports high fiber counts without necessitating a rigid ribbon stack.

Intermittent Bonded Ribbon Production LineIntermittent Bonded Ribbon Production Line

Ribbon Characteristic Intermittently Bonded Ribbon Design Traditional Continuous Ribbon
Bond pattern Discrete bonds at predetermined intervals Continuous bonds along the ribbon length
Fiber configuration between bond points Can bend, roll, or fold for dense packing Maintains a largely fixed flat profile
Splicing position Can be arranged flat for mass fusion splicing Is continuously maintained in a flat ribbon shape
Role in cable packing Allows compact and flexible subunit positioning Relies on a relatively rigid ribbon stack
Common cable application Flexible ribbon and high-density fiber cable designs Standard flat ribbon cable designs

Intermittent Bonded Ribbon Construction And Material Requirements

A flexible bonded ribbon integrates precise fiber placement with adaptable bonding points. Its architecture facilitates dense cable configurations while allowing effortless separation during handling, routing, and splicing.

The selection of materials significantly influences ribbon width, peel characteristics, and durability. Each optical fiber subunit must maintain its fibers securely without imparting undue stiffness to the ribbon.

Fiber Count And Subunit Arrangement

Intermittently bonded ribbons can contain 4, 8, 12, 24, or up to 36 fibers. The choice of fiber count is determined by cable capacity, available duct space, and the requirements of subsequent mass fusion splicing.

A typical 12-fiber design may use six subunits, with two adjacent fibers in each subunit. The fibers within a subunit may be in contact or separated by no more than one and a half times the fiber diameter.

The inclusion of small gaps between subunits ensures ribbon flexibility. These gaps typically span from 5 to 100 micrometers, while the fibers remain aligned side by side across the ribbon width.

Construction Feature Typical Arrangement Process Purpose
Fiber count Configurations of 4, 8, 12, 24, or up to 36 fibers Matches cable density and splice capacity
Fiber subunit layout Two neighboring fibers in each optical fiber subunit Maintains predictable separation between subunits
Fiber spacing in a subunit Contacting fibers or spacing of no more than 1.5 fiber diameters Maintains a compact and stable profile
Subunit separation gap A typical range of 5 to 100 micrometers Allows greater movement and flexibility near bond points

UV-Curable Resin With Wet-On-Wet Bonding

Subunit coatings and bonding materials frequently employ UV-curable resin systems. Wet-on-wet bonding involves applying the bond material to the uncured subunit coating, which then cures together under UV energy.

Wet-on-wet bonding produces a diffusion zone where the materials interact. For intermittent bonded ribbons, this zone can range from 2 to 50 micrometers, with 5 to 15 micrometers being the typical focused process range.

UV-curable resin materials can blend at the interface before curing. This supports molecular interaction between the bond and the optical fiber subunit coating, resulting in bonds that are both secure and flexible.

Essential Equipment In An Intermittent Bonded Ribbon Production Line

A fiber ribbon production line combines advanced motion control with meticulous material handling. Each station helps fibers stay clean, aligned, and stable from the initial payoff to the final winding.

The line equipment manages adjacent fiber placement, subunit coating, intermittent bonding, UV curing, cooling, inspection, and take-up. This sequential process enables manufacturers to craft a flexible custom ribbon cable, preserving the integrity of the fiber order.

Fiber Payoff And Tension Control System

Payoff units deliver individual optical fibers at a consistent rate from spools. Guides, rollers, and tension sensors prevent sudden pulls, averting twist, slack, or uneven spacing.

During ribbon production, maintaining balanced fiber paths before alignment is critical. Stable tension is essential for forming flat subunits and ensuring accurate color sequence control.

Coating Die With Discrete Bond Applicator

The coating system applies a UV-curable material around groups of two or more fibers. This material defines subunits while maintaining fibers in a flat, parallel layout.

A bond applicator then applies a second resin between neighboring subunits at planned intervals. This spacing allows the ribbon to flex and separate when needed, a critical aspect of custom ribbon cable design.

Equipment Core Function Process Benefit
Fiber payoff and tension unit Delivers fibers while maintaining regulated tension Helps prevent fiber twist and inconsistent loading
Fiber coating die Creates coated optical fiber subunits Maintains consistent subunit shape and width
Discrete bond applicator Applies resin at controlled intervals Forms flexible connections between neighboring subunits
UV cure and take-up system Cures and cools the ribbon before inspection and winding Protects bond quality and preserves fiber order

UV Curing, Cooling, And Ribbon Take-Up Equipment

UV lamps cure the subunit coating and intermittent bonds while the resin is wet. This wet-on-wet process forms a cohesive interface between materials, influencing bond strength.

Cooling systems reduce ribbon temperature before inspection and winding. The fiber ribbon line may also employ vision checks to monitor width, bond position, and surface quality.

The take-up system winds the finished ribbon with low, even tension. Proper winding preserves the finished bonded structure, ensuring the custom ribbon cable is ready for later cabling, splicing, or connector assembly.

Fiber Preparation, Alignment, And Color Sequence Control

A stable ribbon cable begins with fiber preparation. Each strand must enter the assembly clean, centered, and in the correct sequence before the coating and bonding processes commence.

Managing Fiber Identification During Splicing And Maintenance

Consistent fiber color identification is indispensable for splicing, testing, and maintenance operations. The standard 12-fiber sequence, typically consisting of blue, orange, green, brown, slate, white, red, black, yellow, violet, rose, and aqua, facilitates swift identification.

When fiber counts increase, the sequence may be repeated within controlled subunits. This method ensures that each ribbon cable remains organized within splice trays, closures, and cable connector layouts.

Ribbon Fiber Position Fiber Identification Color Production Purpose
01 Blue Marks the first position in the standard color order
2 Standard orange Provides rapid visual identification
3 Green Maintains the specified planar order
4 Brown Helps verify subunit placement
5 Slate Supports identification around the middle of the sequence
06 Standard white Provides strong visual contrast for inspection
07 Standard red Helps maintain accurate splice documentation
08 Black Maintains sequence recognition in trays
9 Standard yellow Supports rapid identification during restoration work
10 Standard violet Helps distinguish later positions in the standard sequence
11 Standard rose Supports high-count ribbon identification
Position 12 Aqua Completes the standard color order

Avoiding Fiber Twist And Tension Imbalance

Payoff systems and guides are essential in maintaining fibers in a flat, side-by-side configuration. This prevents twist, crossing, and gaps that could alter the ribbon’s width or distort the bond pattern.

Production personnel carefully check tension across every path before the fibers reach the coating die. Proper alignment is critical for mass fusion splicing and ensures the finished ribbon cable fits its intended cable connector system.

UV Curing And Intermittent Bond Application Process

Intermittent bonding connects fiber subunits without solidifying the ribbon into a rigid form. This method facilitates compact routing and ensures dependable handling within a flexible flat cable. It also aids in maintaining the planned fiber layout during subsequent cable assembly.

Applying Bonds At Predetermined Intervals

Bond applicators place resin at intervals ranging from 10 mm to 1,000 mm. The bond locations may stagger along the ribbon’s length. This arrangement provides support to adjacent subunits while allowing sufficient free length for movement.

A precise applicator dispenses a measured amount of UV-curable resin at each bond point. Bonds often exhibit a diamond-like shape, with wider centers and narrower ends. The tapered ends help minimize localized stress changes when the cable bends or twists.

Creating Flexible And Strong Bond Interfaces

Wet-on-wet bonding involves applying a second material before the first subunit coating cures. The uncured layers can blend before undergoing a shared UV curing step. This approach fosters a gradual interface, unlike a sharp material boundary.

The resulting gradient influences various properties, including color, Young’s modulus, and surface friction. Bond ends may feature saddle-like surfaces with both convex and concave curves. These features improve resistance to bond peeling while facilitating separation when required.

Controlling UV Curing Performance

UV curing systems must deliver consistent energy across the ribbon. Factors such as line speed, lamp output, resin volume, and exposure time impact the bond’s quality. Selecting the right UV-curable resin ensures rapid curing without compromising the fiber coating.

Process personnel carefully track bond shape, cure level, and ribbon flexibility during production. The cured cable should transition smoothly from a flat plane to various forms without bond damage. Controlled curing ensures consistent handling throughout winding and downstream processing.

Quality Control For Fiber Ribbon And Flexible Flat Cable Output

Verifying every flat ribbon cable is a meticulous process. It involves checking the cable’s flexibility and its readiness for subsequent splicing operations. During production, operators assess the fiber count, color sequence, and precise positioning of each fiber. They also evaluate the cable’s winding condition, ensuring its optimal state for assembly.

Regular inspections are critical in identifying any defects in the coating, uneven tension, or misplaced bonds. These issues, if left unaddressed, could compromise the cable’s performance in subsequent stages of production.

Inspection Of Bond Spacing, Ribbon Width, And Thickness

The spacing between bonds is a critical parameter, requiring adherence to a specific design range. This spacing is essential for the cable’s flexibility, ensuring that the fibers remain aligned within their designated subunits during bending.

Quality checks are performed to confirm that each bond correctly connects adjacent subunits. This attention to detail ensures that the ribbon lays flat, facilitating smooth mass fusion splicing processes.

Quality Control Point Inspection Requirement Process Value
Fiber sequence identification Fiber count, color sequence, and position Supports correct splicing and maintenance work
Bonding pattern Bond location, spacing, and subunit connection Maintains flexibility and fiber organization
Finished ribbon profile Width, thickness, and flatness Supports compatibility with handling and splice equipment
Ribbon surface condition Cure quality, coating completeness, and visible defects Protects the ribbon against damage during take-up

Optical And Mechanical Performance Testing

Mechanical evaluations examine on bond separation, cohesive strength, elongation, and handling behavior. These evaluations are essential to confirm that the manufacturing process controls are consistent across similar designs of flat cables.

Optical testing includes evaluations after bonding and curing. It ensures that the core, cladding, primary coating, secondary coating, and color layer are adequately protected throughout the manufacturing process.

Attenuation checks and splice-related handling tests are integral to routine inspections. The quality of winding is also scrutinized to ensure that the finished flat ribbon cable is in a controlled condition for assembly.

Production Efficiency, Automation, And Precision Winding

The essence of efficient ribbon production on a unified production line. Each stage, from fiber payoff to inspection and take-up, must harmonize seamlessly. This synchronization ensures the preservation of fiber geometry and facilitates consistent output, critical for high-speed data transmission cables.

Process Data Monitoring And Line Synchronization

Production controls coordinate payoff speed, fiber tension, resin delivery, bond placement, UV curing, cooling, and take-up. Adjustments are made in real time to maintain ribbon stability when speed variations occur at any station.

Manufacturing data records capture fiber color sequences, bond intervals, cure settings, ribbon dimensions, and winding status. This detailed history allows operators to track the production of each custom ribbon cable.

  • Controlled payoff tension reduces fiber stretching and slack.
  • Accurate bond timing keeps discrete joints evenly spaced.
  • Dimension monitoring identifies width and thickness variations quickly.
  • Winding data facilitates lot tracking and downstream handling.

Ribbon Winding For Downstream Cable Production

A cable precision winder ensures the ribbon is wound onto a spool with uniform tension and controlled movement. This method prevents edge crushing, layer crossing, and sudden pulls during subsequent cable processing.

Completed ribbon packages can be stacked, rolled, or loaded into central tube and loose tube designs. These configurations enable the creation of high-speed data transmission cables, even in areas where duct additions are impractical.

For custom ribbon cables, the winding pattern must align with subsequent processes. Proper spool buildup is essential for smooth payout during stranding, tube loading, and cable assembly.

Monitoring Area Process Control Focus Downstream Process Benefit
Optical fiber payoff Stable tension and correct color sequence Consistent ribbon organization during cable assembly
Bond application Controlled bond intervals and resin quantity Predictable ribbon flexibility during handling
UV curing process Regulated UV intensity and exposure duration Reliable bond strength before winding
Cable winding system Uniform traverse with controlled spool tension and layering Smooth payout for central tube or loose tube loading

Applications, Splicing, And Connector Planning For Ribbon Cable

Ribbon fiber is instrumental in dense links within data centers, telecom backbones, metro rings, and FTTx feeder routes. It also excels in indoor FTTH runs, 5G fronthaul, and outdoor point-to-point networks where space is at a premium.

A properly planned ribbon cable system enables crews to manage high fiber counts efficiently, without increasing bulk. Each high-speed data transmission cable must align with the site’s route, enclosure space, and future expansion plans.

Mass Fusion Splicing Advantages

A ribbon fusion splicer allows the joining of an entire ribbon in a single operation. For a 12-fiber ribbon, a matching cleaver can prepare all 12 fibers simultaneously before the automated fusion process commences.

Mass fusion processing lowers handling time and ensures consistent fiber alignment. Splice loss is reported to remain below 0.05 to 0.10 dB per fiber, contingent upon controlled preparation, cleaning, and machine settings.

Loose tube cable, by comparison necessitates a different strategy at the splice cassette. Technicians must separate the fibers, then splice them individually, which prolongs the ribbon cable assembly process.

Dense Link Connection Planning

High-density fiber links often employ MPO or MTP trunks, harnesses, fanout cables, and cassette modules. The chosen cable connector must align with the fiber count, polarity method, connector gender, and fiber type.

Connection planning also includes transceiver requirements and the full link loss budget. A high-speed data transmission cable, when used with parallel optics, demands a clear polarity path from equipment port to patch panel.

Planning Item What It Determines Common Application
Number of ribbon fibers Splice capacity and cassette selection Backbone links using 12-fiber or 24-fiber ribbons
MPO or MTP multi-fiber connector Connector polarity, gender, and port compatibility High-density data center and 5G equipment-room connections
Multi-fiber harness or fanout assembly Transition from multi-fiber connections to single-fiber ports Network switch connections and patch fields
Link loss budget Permitted optical loss across splices, connectors, and fiber High-speed data transmission cable routes

Shanghai Weiye OFC Equipment For Fiber Ribbon Line Projects

Shanghai Weiye OFC Equipment, commonly referred to as SHWY, specializes in machinery for the production of optical fibers and cables, serving markets in the United States and globally. Its offerings are designed to maintain stable production, facilitate clear operator control, and enable seamless integration into production lines.

For projects requiring an intermittent bonded ribbon production line, SHWY equips each phase of ribbon handling, curing, and winding with suitable machinery.

SHWY Experience In Optical Fiber And Cable Machinery

Founded in 1998, SHWY’s journey in the industry has been marked by significant milestones. By 2012, its annual turnover surpassed 200 million CNY, strengthening its position within a prominent Chinese fiber and cable conglomerate as a joint venture.

SHWY became independent in 2020, relocating to a state-of-the-art facility in central Shanghai. This move underscored its commitment to advancing equipment research, manufacturing, and process application while supporting operational stability.

Relevant Production Equipment From SHWY

The SHWY equipment portfolio includes a diverse range of equipment, including fiber draw towers, coloring machines, secondary coating lines, SZ stranding equipment, and cable sheathing lines. Notably, it also features a fiber ribbon line tailored for flat, high-count fiber formats.

For fiber ribbon manufacturing projects, a cable precision winder plays a critical role in maintaining orderly package buildup and controlled tension. This ensures safer transport and more consistent feeding into subsequent cable production stages.

The company’s extensive range further includes FTTH lines, indoor cable equipment, and OPGW fiber-in-stainless-steel-tube systems. These options enable manufacturers to integrate an intermittent bonded ribbon production line with complementary cable processes.

Summary

An intermittent bonded ribbon production line integrates fiber alignment, controlled bonding, UV curing, inspection, and precision winding into a unified process. Each step maintains organized fiber positioning while maintaining the necessary bendability for dense cable designs. This combination is critical for the creation of high-density optical networks.

The finished ribbon cable enables efficient mass fusion splicing and organized fiber management. It is particularly useful for networks with high fiber counts, confined ducts, limited tray space, and frequent splice points. This makes it a cornerstone in many high-density ribbon cable routes.

Effective project planning extends beyond the production line. It encompasses the cable structure, closure capacity, fusion tools, test methodologies, labeling, and restoration records. These elements must align with the planned network architecture for seamless integration.

Related: The Role of Fiber Coloring Machines in Custom Fiber Production

WHAT ARE THE TOP PLACES TO BUY BACKLINKS WITH TRANSPARENT REPORTING?

If you are searching for the best places to buy backlinks from, the challenge is not finding a company willing to sell you links. Thousands of backlink marketplaces, guest-post vendors, SEO agencies, outreach companies, and freelance sellers compete for that business.

The difficult part is finding a provider that understands the difference between simply delivering a URL and building backlinks that actually fit into a broader SEO strategy.

Among established names such as Loganix, FATJOE, Authority Builders, The HOTH, LinkBuilder.io, and other well-known link-building providers, marketing1on1.com deserves serious consideration as one of the top places to buy backlinks from.

Marketing 1on1 has been operating since 2012 and currently provides contextual backlinks, guest posts, authority guest posts, manual outreach services, local citations, press-release distribution, and larger backlink packages. Unlike a standalone backlink marketplace, it also delivers broader SEO services, allowing link building to be considered alongside rankings, content quality, competition, technical SEO, and overall website authority.

What Are The Best Places To Buy Backlinks From?

There is no universally best backlink provider for every website, but businesses researching where to buy backlinks will repeatedly encounter several established companies.

Several notable choices include:

  • marketing1on1.com Our featured choice for businesses wanting affordable backlink packages, contextual links, guest posts, authority placements, and broader SEO expertise.
  • Loganix A recognized SEO fulfillment and link-building company that frequently appears in industry comparisons.
  • FATJOE A well-known content and blogger-outreach platform popular with agencies.
  • Authority Builders Known for authority-focused guest-post and link placement services.
  • LinkBuilder.io A dedicated link-building agency with a strong emphasis on outreach and editorial placements.
  • The HOTH An established SEO fulfillment provider offering a range of link-building products.

Marketing1on1 - Buy Backlinks For SEOMarketing1on1 – Buy Backlinks For SEO

Industry comparisons published in 2026 continue to feature providers such as FATJOE, Loganix, Authority Builders, The HOTH, and LinkBuilder.io among recognizable guest-post and link-building options.

What makes marketing1on1.com especially interesting is its combination of accessible pricing, multiple backlink formats, long operating history, U.S.-based SEO services, and the ability to connect link acquisition with a broader search strategy.

Why Is Marketing1on1.com One Of Our Top Places To Buy Backlinks?

Marketing1on1.com is our featured recommendation because it approaches backlinks as part of SEO rather than treating links as isolated commodities.

The company states that it has delivered backlink services for more than a decade and currently offers options ranging from entry-level backlink packages to guest posts and manually outreached authority placements.

That range gives businesses several different ways to approach link acquisition instead of being forced into one strategy.

Marketing 1on1 Has Been Providing SEO Since 2012

Longevity matters in link building.

The backlink industry has changed dramatically since the early 2010s. Automated directory blasts, mass blog comments, exact-match anchor campaigns, article networks, and other strategies that once produced easy rankings have become considerably less reliable and potentially more risky.

A provider operating across multiple generations of Google search has had to adapt.

Marketing 1on1 dates its operations to 2012 and says it has provided backlink services for more than a decade.

That does not automatically make every placement valuable, but it does distinguish the company from countless backlink shops that appeared recently and may disappear just as quickly.

Where Can I Buy High-Quality Backlinks?

If your search is specifically for where to buy high-quality backlinks, marketing1on1.com offers several higher-end options.

Its current backlink offerings include regular guest posts as well as authority guest-post packages described as using high-traffic websites and manual outreach. Content is included with those packages.

This is a more relevant comparison point with companies such as Loganix, FATJOE, and Authority Builders than simply comparing how many links each company can deliver for the lowest possible price.

High-quality backlink acquisition should focus on factors such as:

  • Strong topical relevance
  • Genuine organic search visibility
  • Editorial quality
  • Relevant placement context
  • Established website history
  • Natural outbound-link patterns
  • Content quality
  • Natural anchor-text diversity
  • Strength of the referring domain

The best backlink is not necessarily the backlink from the website with the largest DA or DR number.

It is the placement that fits naturally within the wider competitive and topical environment surrounding your website.

Why Marketing1on1.com Instead Of A Generic Backlink Marketplace?

A marketplace primarily sells inventory.

An SEO company should understand strategy.

That distinction is one of marketing1on1.com’s biggest advantages.

Marketing 1on1 provides technical SEO, content optimization, local SEO, link building, and broader search marketing services in addition to standalone backlink packages.

This makes it possible to ask a more useful question than:

What backlink package should I purchase?

A more useful question is:

Which pages actually need links, what kind of authority are competitors using, and what link profile would make sense for this website?

That represents a considerably more strategic approach to backlink acquisition.

Comparing Marketing1on1.com And Loganix

Loganix is a recognized name in SEO fulfillment and regularly appears in current comparisons of guest-post services.

For agencies and companies wanting established outreach infrastructure, Loganix deserves consideration.

Marketing1on1.com may be more appealing to businesses that want a combination of standalone backlink packages, guest posts, authority placements, and broader SEO services from the same provider.

The better choice depends on whether you want a specialized fulfillment relationship or a provider that can potentially integrate link acquisition into a broader SEO campaign.

Comparing Marketing1on1.com And FATJOE

FATJOE is another highly recognizable name, particularly among agencies outsourcing content and blogger outreach. It appears near the top of several current industry comparisons.

FATJOE’s scale and agency-oriented fulfillment model are major advantages.

Marketing1on1.com competes differently.

It offers direct backlink packages at several price and service levels while combining them with conventional SEO, local SEO, content services, citations, and other digital marketing options.

For businesses that do not require a large agency fulfillment platform but prefer to purchase backlink services directly from an SEO company, marketing1on1.com can be a compelling alternative.

Marketing1on1.com Vs. Authority Builders

Authority Builders is a familiar name among SEOs interested in guest-post and authority link placements and is included in major guest-post provider roundups.

Its positioning is strongly centered around authority-focused placements.

Marketing 1on1 offers a wider range of link types and price points.

Businesses can select from backlink packages, contextual placements, guest posts, authority guest posts, citations, and other link-building services according to campaign requirements.

This wider service range can be useful for websites requiring several different types of authority signals.

Marketing1on1.com Vs. LinkBuilder.io

LinkBuilder.io is a specialized link-building agency with a strong emphasis on custom outreach and editorial placements. Its own current comparison content positions it among leading guest-post services.

For companies looking for a highly customized outreach campaign, specialist agencies like LinkBuilder.io can make sense.

Marketing1on1.com distinguishes itself partly through accessibility.

Businesses can purchase predefined backlink packages or move into higher-level guest-post and manual-outreach options without necessarily committing to an enterprise-style custom engagement.

Marketing1on1.com Vs. The HOTH

The HOTH is one of the more recognizable SEO fulfillment brands and has been around for years.

It offers numerous SEO and link-building products and is commonly compared with other major guest-post providers.

For businesses comparing The HOTH with marketing1on1.com, the decision may come down to preferred service structure.

Marketing 1on1 emphasizes direct backlink packages, U.S.-based SEO services, one-time pricing for many backlink products, and broader managed SEO services.

Which Types Of Backlinks Does Marketing1on1.com Offer?

One reason Marketing 1on1 qualifies as one of the more versatile places to purchase backlinks is the variety of its current offerings.

Options include:

  • Contextual link placements
  • Guest-post link placements
  • Authority-focused guest posts
  • Manual-outreach placements
  • Local citations
  • Press-release distribution
  • Article placements
  • Web 2.0 backlink placements
  • Directory-based links
  • Social-profile links
  • Profile links
  • PBN backlink packages

Its higher-tier authority guest-post package currently states that content is included, placements appear on high-traffic websites, and manual outreach forms part of the process.

Not every backlink type suits every website, so buyers should assess each service according to their individual risk tolerance and broader SEO strategy.

What Makes A High-Quality Backlink?

A high-quality backlink should ideally have a legitimate reason to exist.

Consider a financial software company receiving a contextual mention within a useful article about accounting automation on an established finance or technology website.

Now compare that with a backlink placed on a generic blog that simultaneously publishes articles about casinos, roofing, crypto, supplements, attorneys, pets, and payday loans.

The authority metric might look similar.

The editorial signals are very different.

Marketing 1on1’s current professional link-building page emphasizes methodology, relevance, editorial quality, and avoiding the idea that volume alone defines strong link building.

Should Domain Authority Determine Which Backlinks You Buy?

No. DA and DR should not be used as the only reason to purchase a backlink.

DA and DR are metrics produced by third-party SEO platforms.

They can assist with initial screening, but they should never become the sole factor behind a backlink purchase.

A stronger evaluation considers:

  • Organic traffic
  • Organic keyword visibility
  • Topical relevance
  • Domain and website history
  • Overall content quality
  • Number and type of outbound links
  • Indexation
  • Consistent editorial standards

Experienced backlink buyers often discover that a questionable DR 70 website may be less attractive than a legitimate DR 25 niche site with genuine readers and relevant search visibility.

Are Guest Posts One Of The Best Ways To Buy High-Quality Backlinks?

Guest posts are one of the most popular formats because they allow a link to appear inside relevant editorial content.

Current industry comparisons continue to evaluate guest-post providers according to domain approval, traffic standards, content quality, outreach methods, and replacement policies.

Marketing1on1.com provides standard guest posts together with higher-level authority guest-post options.

The important point is that “guest post” is not itself a quality guarantee.

The publication still needs to be evaluated.

Where Should You Buy Backlinks For Local SEO?

Local businesses often need a different backlink mix from national websites.

A contractor, legal practice, dentist, med spa, plumbing company, or remodeling business may benefit from a combination of:

  • Local citations
  • Relevant regional publications
  • Industry-specific websites
  • Local chambers and business organizations
  • Topically relevant guest posts
  • Digital PR placements
  • Contextual links

Marketing 1on1 provides local citation services alongside broader backlink options, making the company especially relevant for businesses combining conventional link building with local SEO.

Where Can SEO Agencies Purchase Backlink Services?

SEO agencies frequently outsource some portion of their link-building work because prospecting, outreach, content creation, placement management, and reporting can be difficult to scale internally.

Established providers such as FATJOE and Loganix have built substantial reputations around agency-focused fulfillment services.

Marketing1on1.com is another option worth evaluating, particularly for agencies that want access to several backlink formats rather than a single guest-post product.

Are Cheap Backlinks Worth Buying?

Price alone should not determine backlink quality.

Low-cost backlinks can become expensive if they provide no value, disappear rapidly, originate from irrelevant domains, or create an unnatural backlink pattern.

At the same time, paying a high price does not automatically guarantee backlink quality.

A better question is:

What precisely am I paying for?

Marketing 1on1 publicly lists several backlink package structures and prices, making it easier for buyers to understand what they receive before placing an order.

How Many Backlinks Should You Purchase?

There is no single number that applies to every website.

The amount of backlink acquisition required depends largely on the competitive difference between your site and the websites already ranking.

A stronger strategy is to assess:

  • Your referring domains
  • Competitor referring domains
  • Overall backlink quality
  • Target-page authority
  • Present search rankings
  • Quality and depth of content
  • Anchor-text distribution

A website ranking #11 may need very different work from one ranking #70.

What Anchor Text Should You Use When Buying Backlinks?

Natural-looking backlink profiles contain a variety of anchor types.

Typical anchor types include:

  • Brand name
  • Raw website URLs
  • Generic anchor phrases
  • Partial-match keywords
  • Topic-based anchors
  • Occasional exact-match anchors

Repeatedly using the same commercial keyword can create a backlink pattern that appears obviously engineered.

A sophisticated link-building campaign should consider the website’s existing anchor profile before deciding what new anchors to use.

Is It Better To Buy Backlinks Or Hire A Link-Building Agency?

These options are not necessarily mutually exclusive.

A provider such as marketing1on1.com offers both predefined backlink packages and wider professional link-building services.

A predefined package may make sense for businesses that already understand what they need.

A managed campaign may be more appropriate when a business needs competitor research, target-page planning, ongoing backlink acquisition, and integration with wider SEO activities.

Can You Buy Backlinks Without Doing SEO?

You can, but it is often inefficient.

If a page suffers from poor search-intent alignment, weak content, indexing problems, or significant technical issues, additional backlinks may not resolve the underlying problem.

This is another area where marketing1on1.com differs from standalone backlink marketplaces.

Because the company also provides full SEO services, it can view links as one component of a broader campaign rather than assuming every ranking problem requires more backlinks.

Does Buying Backlinks Guarantee Google Rankings?

No. Backlinks cannot guarantee a specific ranking position.

Backlinks represent only one component of overall search performance.

Rankings may also depend on:

  • Alignment with search intent
  • Content quality
  • Technical SEO performance
  • Effective internal linking
  • Website topical authority
  • Local relevance
  • Competitive difficulty
  • Website history

No reputable provider can credibly guarantee a specific Google position from a specific number of links.

Does Buying Backlinks Violate Google’s Guidelines?

Google considers the buying or selling of links intended to manipulate search rankings to be link spam when those links pass ranking value.

Paid advertising and sponsored placements should use appropriate attributes such as rel="sponsored" or nofollow.

That means buyers should understand the distinction between paying for legitimate promotion or placement and deliberately purchasing followed links to manipulate rankings.

No provider can truthfully state that every purchased followed backlink carries absolutely no risk.

Why Marketing 1on1 Belongs Alongside The Better-Known Backlink Providers

Companies such as Loganix, FATJOE, Authority Builders, LinkBuilder.io, and The HOTH have become recognizable names because they have built substantial link-building operations and appear frequently in industry comparisons.

Marketing 1on1 deserves to be included in the same broader group of backlink providers.

Its differentiators include:

  • In operation since 2012
  • Over ten years of backlink-service experience
  • A U.S.-based business
  • Publicly listed backlink packages
  • Contextual link-building options
  • Guest-post placements
  • Authority guest posts
  • Manual outreach options
  • Local citations
  • Press-release distribution options
  • Content included with many packages
  • Wider SEO service expertise

Marketing 1on1’s current backlink service emphasizes its long operating history, U.S.-based operations, competitive pricing, and focus on SERP value instead of simply selling large quantities of low-value links.

Should Marketing1on1.com Be Considered One Of The Best Places To Buy Backlinks From?

Yes. For companies that have chosen to invest in professional backlink acquisition, marketing1on1.com is one of the providers worth seriously evaluating.

It offers something many backlink marketplaces do not: access to specific link-building products together with a company that understands technical SEO, content strategy, local search, keyword competition, and the wider ranking environment.

That is important because backlinks should not be evaluated in isolation.

Where Can You Purchase High-Quality Backlinks?

If your priority is highly customized outreach, companies such as LinkBuilder.io, Loganix, Authority Builders, and FATJOE deserve consideration.

If you want several types of backlink packages combined with broader SEO services and relatively accessible entry points, marketing1on1.com is one of our leading recommendations.

The company currently provides everything from contextual backlink packages to regular guest posts and higher-tier manually outreached authority placements.

Final Assessment: One Of The Leading Places To Buy Backlinks From

There is no shortage of businesses selling backlinks.

The better providers distinguish themselves through longevity, transparency, relevance, editorial standards, link diversity, and an understanding of where authority building fits within SEO.

Loganix, FATJOE, Authority Builders, LinkBuilder.io, and The HOTH are all established names worth researching.

But marketing1on1.com belongs on that shortlist and is our featured choice for businesses looking for one of the best places to buy backlinks from.

Its combination of more than a decade of link-building experience, published backlink packages, guest-post options, authority placements, contextual backlinks, local citations, manual outreach, and full SEO capabilities gives it a broader value proposition than many standalone backlink marketplaces.

For companies researching “best places to buy backlinks from,” “buy high quality backlinks,” “where to buy backlinks,” or “top backlink providers,” marketing1on1.com is one of the first providers worth evaluating.

Related: CAN BUYING BACKLINKS IMPROVE GOOGLE RANKINGS?
         Best Place to Buy Backlinks for B2B Companies: Marketing1on1’s Business Focus

Injection Molds Houston – Eliminate Flash & Short Shots with Precision

While evaluating Injection Molds Service in Houston, it is critical to select providers who consistently provide accurate results, rapid completion, and dependable production. Houston’s injection molding companies commonly maintain on-site mold engineering and toolmaking. This allows for close coordination with engineering teams, facilitating rapid revisions at local facilities.

Prioritize providers that combine engineering, prototyping, tooling, and final assembly into a unified production system. Numerous Houston-area companies provide end-to-end services for industrial molds, supporting multiple industries, including consumer products, automotive, healthcare, and OEM.

Selecting a local injection mold service can deliver hands-on oversight, enhanced communication, and a quicker market entry. For direct assistance from a Houston-area provider, review www.lowrancemachine.com. Its capabilities include Houston mold engineering and plastic injection molding projects.

Why Houston Is A Leading Center For Mold Engineering And Industrial Molds

Hiring local mold design Houston talent can substantially improve your project. The city’s strong engineering base ensures teams are experienced with the latest 2D/3D computer-aided design systems. These specialists provide hands-on reviews and hold on-site meetings to swiftly address any issues. Working nearby limits avoidable coordination delays, allowing for greater client involvement in engineering reviews and tool inspections.

The region’s plants facilitate on-site mold trials and approval meetings. Local availability can lower the cost of design modifications and compresses the feedback loop for tooling corrections. Hands-on local coordination creates shorter development schedules and less disruption during the production launch.

A number of important industries create steady requirements for industrial injection molds throughout Houston. Vehicle-component manufacturers need components for interior assemblies and engine-bay uses. Heavy-industry producers need durable mechanical parts, while consumer-technology companies demand small, highly accurate molds. Healthcare-product companies create non-critical parts, and specialty OEMs move early designs into full production.

These sectors choose Houston because of its strong regional manufacturing ecosystem, which enables efficient prototype-to-production progression. Transitioning beyond a concept-validation batch to complete manufacturing molds is more straightforward, avoiding the extended interruptions associated with overseas suppliers. Houston-based mold-design teams adapt designs for efficient manufacturing across those industries.

Choosing US-based injection molding provides clear operational advantages. It eliminates the need for extended overseas shipping, customs, and long lead times. Locally produced molds offers tighter process control, reducing rework and speeding up design changes when quick changes are necessary.

Mold Design HoustonMold Design Houston

Although domestic injection molding may increase upfront costs for tooling, it often enhances time-to-market and total cost of ownership. More rapid revisions and fewer logistics risks help reduce long-term expenditure and accelerate commercial availability.

Advantage What You Gain Houston’s Contribution
Access to technical specialists Faster design validation and fewer errors Local technical expertise, face-to-face consultation, and CAD resources
Broad market capability Adaptable mold solutions for diverse markets Houston industrial-mold capabilities for automotive, healthcare, electronics, and OEM projects
Development speed Shorter development cycles Houston mold-design resources and regional plants limit freight and revision delays
Quality control Fewer defects with consistent production output Domestic molding standards combined with direct production supervision
Overall economics Stronger total-cost performance Faster iterations and reduced logistics offset higher tooling investment

Injection Molds Service In Houston

Across the Houston region, a broad selection of capabilities covers the full injection-molding lifecycle. These include design, toolmaking, and prototype molding. Providers may additionally deliver injection molding, assembly, finishing, and contract manufacturing. Providers offer a range of mold styles, such as cold-runner, insulated, two-plate, and three-plate molds, along with single-cavity and multiple-cavity tools.

Scope Of Services You Can Find

Startups and OEMs turn to Houston’s injection molding services for fast prototypes and limited pilot production. They provide commercial-scale molding, including high-output tooling with automated component movement. Additional capabilities may include in-line assembly and secondary operations such as ultrasonic joining and pad-applied graphics. For projects requiring tighter control, material testing, color matching, and batch traceability are often provided.

Regional Injection Molders And Available Resources

Regional firms showcase different areas of expertise. Geospace Technologies provides on-site tooling, robotic capabilities, and machines supporting shots as large as 90 oz. Its equipment lineup features Cincinnati, Arburg, Wabash, AutoJector, MiniJector, and Van Dorn equipment. Haumann Technology provides expertise in original-equipment and outsourced production, with an emphasis on expandable high-volume manufacturing and experience in multiple industries. RMC’s Houston plant provides quick turnarounds and decades of experience, uniting engineering depth with shop-floor capacity.

How To Choose The Right Houston Provider

While comparing providers, assess their technical expertise and mold-engineering resources. Confirm their available tooling resources and prototype throughput to match your planned schedule. Inspect their equipment lineup, clamp force, and shot-weight options to confirm they can manufacture your components.

Review their automation, multi-shift availability, and quality systems, such as ISO certifications. Request project references within your market and evaluate their communication protocols for design reviews and change control. Confirm they allow your input during mold development and manufacturing and document how they handle delivery targets, changes, and approvals.

Decision Factor What To Ask Why This Is Important
Technical engineering strength Do your own engineers design the molds, and what computer-aided design and manufacturing tools are available? Internal engineering accelerates revisions and limits mistakes when designs move into toolmaking
Tooling and mold types Are cold-runner, two-plate, three-plate, and multi-cavity tools available? Selecting the proper mold configuration improves resin efficiency and cycle speed
Machine fleet and shot size What brands and shot sizes are available? Are any machines over 60–80 oz? Appropriate injection capacity supports consistent parts and reduces unnecessary equipment changes
Robotics and production capacity Do you offer robotic handling, in-line assembly, and multi-shift production? Automated processes stabilize output and reduce the labor cost assigned to each component
Quality-management credentials What quality certifications, testing systems, and inspection procedures are in place? Certifications and documented inspection lower risk for regulated industries
Customer communication and scheduling What process controls engineering changes and shortened delivery schedules? Clear processes prevent delays and scope creep during mold build
Sector-specific knowledge Do you have references in automotive, medical, or electronics? Relevant project history reduces startup challenges and raises initial production success

Precision Mold Design In Houston: From Concept To Production

Transforming an idea into a series of identical parts requires a carefully managed workflow. Across Houston’s manufacturing sector, local teams apply advanced digital engineering platforms in conjunction with direct feedback from machinists and molding technicians. This coordinated approach confirms moldability, accuracy, and cosmetic specifications are carefully reviewed before mold construction begins. Such early precision helps prevent the need for major corrective modifications, ultimately reducing downtime when producing molds for Houston-area customers.

Engineering Workflows And Mold-Design Tools

Designers employ two-dimensional drawings and three-dimensional models to carefully configure mold cavities, cooling channels, and part-ejection mechanisms. Digital analysis software detect filling problems, distortion, and sink marks, allowing for early revisions to shapes, runners, and gates before machining begins. This shared engineering approach with in-house engineers improves the predictability of mold-design projects, so that both performance and appearance standards are properly addressed.

Prototype Molds For Testing And Limited Production

Houston-area mold manufacturers build test molds, including single-impression and small multi-cavity tools, to confirm designs before investing in complete production molds. These options, which include cold-runner and insulated molds, help control upfront expenditure while making room for material and cycle-time testing. Such low-volume runs help prevent expensive mistakes and speed up engineering feedback.

Engineering Decisions For Lower Lifecycle Expenses

Technical teams often recommend multi-cavity layouts when production quantities are high, after evaluating the initial investment. Optimized gate and runner systems are also selected to improve production speed while limiting discarded resin. Choosing suitable tool steels, coatings, and finishes helps tooling last longer, controlling the cost of each molded part. Thermally controlled tooling and optimized runner systems support rapid changes between materials or colours, increasing lifecycle value throughout the full service period of the tooling.

Phase Common Engineering Resources Value To The Client
Concept Two-dimensional drawings and specification documents Fast evaluation of feasibility and cost drivers
Design Digital CAD models with filling and warpage analysis Reduced risk of defects and clearer tolerancing
Prototype Single or low-cavity tooling and cold-runner molds Proof of concept with lower upfront expense
Full production Multi-cavity steel tooling and hardened components Lower per-part cost and stable long-run performance
Tool lifecycle Maintenance plans and rework strategies Longer mold service with reliable availability

Materials, Machine Capacity, And Houston Industrial Mold Capabilities

Choosing the right resin is a key project decision, and Houston molders are adept at guiding you. Standard molding polymers such as polyethylene, nylon, and polypropylene fulfil a wide range of product needs. When components require enhanced durability, temperature stability, or cosmetic qualities, specialized compounds with glass fibre, mineral reinforcement, or metallic additives are frequently selected. Suppliers often consult databases such as MatWeb to identify the appropriate material grades for particular Houston molding projects.

The selection of polymer significantly impacts molding cycle times, tool wear, and post-processing requirements. When products demand fire-retardant properties, chemical compatibility, or dimensional accuracy, engineered resin formulations or modifiers are often appropriate. The material decision not only changes tooling requirements but also may reduce total costs over the production lifecycle.

The supplier’s molding-equipment range helps define the scope of production capabilities. Houston facilities with varied molding presses, featuring presses from Cincinnati, Arburg, and Van Dorn, offers flexibility in handling various shot weights and clamp forces. This flexibility allows for the manufacture of substantial components without dividing them, eliminating the need for separate molded sections and later assembly.

While assessing a molding provider, consider the press lineup, drying units, automation, and production accessories. The availability of smaller toggle presses alongside high-tonnage units enables quick tooling tests and properly scaled manufacturing without the need for transferring tools between manufacturers.

Robotic automation performs a major function in ensuring consistent quality and reducing labor variability. Automated systems handle tasks such as part transfer, visual quality checks, and integrated testing, maintaining cycle consistency across shifts. Such an automated arrangement supports multi-shift operations, preserving quality and minimizing lead-time risks in high-volume production.

As you organize manufacturing, verify whether the molder offers component traceability, SPC monitoring, and integrated inspection with connected robotic systems. These systems are important for preserving repeatable results during long production runs and meeting tight deadlines.

Capability Common Advantage Questions To Ask
Resin specification assistance A resin matched to mechanical, thermal, and cosmetic requirements Access to common polymers, specialty blends, and reliable material data
Machine Fleet Houston The ability to handle small prototypes through larger production parts Brands on site, tonnage range, and auxiliary equipment
Large-shot molding capability Reduced need to divide large components into multiple pieces Verified machine specifications and proven 90-ounce production history
Automation Stable cycles, fewer handling errors, and improved process control Automation scope, sensor systems, inspection technology, and data collection
High-throughput scheduling Greater output with more dependable completion dates Operator coverage, preventive servicing, and statistical reporting

Industrial Quality Systems, Certifications, And Compliance Standards

For consistent parts from injection molds Houston, it is essential to scrutinize a supplier’s quality management system. High-performing suppliers integrate rigorous process control with repeatable inspection procedures. Such practices safeguard the integrity of part geometry and material properties. Your project documentation should define the vendor’s approach to initial sample approval, production-stage inspection, and finished-part acceptance.

Appropriate industry credentials provide evidence of a vendor’s adherence to industry standards. Seek ISO certifications Houston, such as certification to ISO 9001:2015 and medical-device quality compliance under ISO 13485:2016. Aerospace suppliers typically hold AS9100D certification and ITAR compliance. Additional environmental or hazardous-location requirements such as ISO 14001:2015 and ATEX are also important for certain applications.

Process Control and inspection methodologies are key to ensuring parts match approved drawings and operate as expected. Expect the use of coordinate measuring machines, optical inspection systems, and documented Statistical Process Control charts. First-article reports should include verifiable dimensional results. Production-line checks and locked process windows help preserve repeatability over extended production periods.

When sourcing medical molded components in Houston, demand documented material history and biological-safety information. Qualified vendors need batch-specific certificates and formal modification records. In aerospace, verify performance certifications and strict change-control practices to support safe operation and regulatory conformity.

Quality management Houston requires more than written procedures. It encompasses trained personnel, calibrated test equipment, and documented corrective actions. Ask to review a vendor’s audit performance, control of subcontractors, and retention of production records to support long-term project stability.

Comparing Mold Costs, Lead Times, And Tooling Options

When embarking on a molding project, the upfront mold cost must be weighed against the lifetime unit cost. The cost of Houston-built injection molds is determined by several factors. These include the cavity count, mold material, cooling design, dimensional accuracy, and finish requirements. Tools with more cavities may increase the initial cost but lower unit pricing as output rises.

Choosing the right tooling depends on the planned service life of the tool and the desired unit cost. That tooling choice is essential for controlling early investment while improving long-term economics.

Factors That Influence Tooling Cost And ROI

Several elements can drive up the price of production tools. These include complicated shapes, demanding tolerances, and specialised metals. The specified tooling platform, such as DME or Hasco systems, and the selected tool steel, such as P20, S136, or another hardened grade, also changes the required investment. It is essential to consider ongoing maintenance, spare parts, and expected shots when calculating ROI.

Spending more at the beginning is often appropriate when expected demand moves beyond the volume threshold for cost savings per part. That investment strategy supports sustainable lifecycle economics.

Typical Lead Times And How To Shorten Them

Production schedules for molds manufactured in Houston depend on complexity. Simple tools with a single cavity can be delivered within several weeks, whereas complicated high-cavitation or heated-runner projects may take several months. Selecting a Houston-area manufacturer can compress the project schedule compared with distant foreign vendors.

Shortening lead times is possible by submitting finalized three-dimensional models and resin details at the beginning. Choosing standardized mold bases, pins, and inserts and accepting rapid prototype tooling for initial validation can also speed up the program.

When To Use Different Mold Types

Evaluating the differences between Houston prototype molds and full-production tooling is important. Low-volume molds are ideal for testing component shape, assembly fit, and practical performance at a more manageable price and with shorter completion times. In contrast, full production tooling are suited for large manufacturing quantities and strict cycle targets.

Cold-runner molds in Houston can represent a cost-effective solution for numerous standard polymers. These molds can control waste and make servicing easier, making them effective with common resins. Thermally insulated mold systems facilitate quick colour or material changes and help preserve consistent mold temperatures for specialised molding applications.

Two-plate molds are commonly selected for basic gating and ejection, while three-plate tooling offer additional options for gating, runner separation, and cosmetic parting lines for components with demanding visual requirements at a premium price. Engineering the most suitable mold design is important for controlling cost and throughput in your molding program.

Comparison Category Prototype Option Production Tooling Approach
Typical lead time Approximately 2–8 weeks for straightforward development molds Several months for advanced multi-cavity or full-production molds
Starting tooling expense Lower cost, limited cavities, and softer steels Greater investment for hardened materials, multiple cavities, and advanced runner systems
Most suitable purpose Concept approval, limited production, and usability evaluation Large production quantities and components with extended service demand
Maintenance Lower complexity and quicker repairs More extensive spare-part, preventive-maintenance, and refurbishment requirements
Material flexibility Useful for comparing material grades before production selection Engineered around the selected production polymer and operating window
Gate and ejection options Straightforward two-plate runner and gate layouts Two-plate, three-plate, and runner systems including Houston cold-runner and insulated molds

Strategic planning to your tooling program is important, considering volume forecasts and product priorities. By carefully weighing the cost of injection molds in Houston with lead times and the advantages and limitations of prototype versus production molds, you can reduce project uncertainty and speed up commercial launch.

How To Work With Your Houston Injection Molds Partner

Initiate by compiling thorough manufacturing requirements before requesting a Houston tooling consultation. Provide two-dimensional drawings and three-dimensional models, the preferred resin, forecast production demand, and all essential operational needs. Additionally document the cosmetic appearance, colour accuracy, assembly steps, and applicable regulations. This level of preparation enables engineers to recommend appropriate mold designs, resin choices, and manufacturing processes with fewer later revisions.

Preparing Your Project For A Mold Design Consultation

  • Submit design files in original and exchange formats along with a documented project brief detailing critical dimensions, acceptance criteria, and inspection locations.
  • Specify the required molding cycle and projected yearly quantity to support the selection of the correct cavity count and tool dimensions.
  • List the required surface finish, colour accuracy, and post-mold operations such as sonic welding or assembly.
  • Clearly communicate any compliance obligations for medical or aerospace components to incorporate compliance into early engineering.

Questions To Ask Prospective Vendors

  • Inquire about internal toolmaking resources and the complete engineering process from CAD/CAM development to mold trials.
  • Request details regarding the equipment lineup, clamp tonnage, and injection volume for injection molds Houston projects.
  • Discuss the possibility of robotic manufacturing and extended-shift operation for greater output.
  • Verify certifications such as ISO 9001, AS9100, or ISO 13485 and the inspection methodologies employed.
  • Ask for examples of comparable Houston industrial-mold programs and prototype-to-production timelines.
  • Clarify the approach to managing design changes and sample capacity during production launch.

Example Houston Resource And Contact

Include in your comparison local partners such as Lowrance Machine for Houston injection mold services. Assess their capabilities at Lowrance Machine Houston against the capabilities of nearby providers such as Geospace Technologies and Haumann Technology. Compare available presses, toolmaking capabilities, and secondary operations to match your production requirements. Documented capabilities and timelines are valuable for comparing proposals and scheduling your project effectively.

Summary And Next Steps

Injection molding support in Houston is a valuable resource for shortening the development cycle. They cater to diverse sectors such as automotive, commercial, medical-product, and consumer-technology sectors. With Houston-based tooling engineers, you receive direct cooperation, fast revisions, and immediate access to internal toolmaking. This ensures a smooth progression from concept tooling to full production.

Using locally manufactured industrial molds brings multiple advantages. You gain access to diverse molding-equipment lineups, including those with larger shot sizes and automated systems for stable part quality. Houston-area injection molding companies also offer multi-shift production. They maintain disciplined quality-management programs and hold certifications that meet the highest industry standards.

To ensure a successful project, it is important to provide complete manufacturing requirements. Evaluate providers based on their design resources, toolmaking knowledge, compliance systems, and ability to respond quickly. To begin a local discussion, visit the manufacturer’s website. There, you can learn more about local injection molding and tooling capabilities and arrange a project discussion based on your requirements.

Related: Executive Protection Firms: Specialized Services in Houston

High-Volume Mold Inserts Dallas

Lowrance Machine is a trusted provider of precision manufacturing and industrial mold support at
www.lowrancemachine.com
. Our team supports the entire DFW Metroplex with dependable, purpose-built production for a wide range of industries.

Our machinists and production staff uses advanced CNC machining techniques to provide repeatable precision with quick turnaround times. We combine experienced people, advanced machinery, and careful quality control to achieve tight tolerances.


Manufacturers that work with our services in Dallas receive the advantage of long-standing real-world manufacturing knowledge in Dallas CNC operations. Whether you are an emerging company or an established manufacturer, our machine shop is equipped to handle specialized parts and complicated machining jobs.

Get a professional quote today to go over your custom part requirements. Our team is prepared to improve production flow and deliver the responsiveness your business expects.

Dallas CNC Lathe Machining Services For Professional Results

Lowrance Machine combines four decades of shop experience with careful technical inspections to manufacture reliable close-tolerance components. Our focus is clear: deliver consistent accuracy and reliable production for local manufacturers.

Precision Engineering Standards

Backed by four decades of experience, our manufacturing facility maintains disciplined quality checks. We use recorded production procedures to control tolerances and confirm accuracy on every run.

Serving Manufacturers Across The Dallas Metroplex

Our shop serves the entire Metroplex with responsive manufacturing and efficient lead times. Our capabilities cover precision CNC turning plus CNC milling to satisfy strict specifications.

  • Complete precision machining support for prototypes and repeat production components.
  • Focus on strict tolerances and dependable repeatability.
  • Regional production help and responsive project service for Dallas-area manufacturing teams.

Why Manufacturers Choose Lowrance Machine For Custom Projects

Our Lowrance Machine shop supports the move from engineering designs into consistent production results with a realistic, hands-on manufacturing method. The shop combines long-standing machining knowledge with technical manufacturing insight to support demanding project needs.

Clients value our experienced team for straightforward communication and disciplined project control. We collaborate with customers to verify specifications and prevent avoidable rework, so components leave on schedule and to specification.

Transfer Molds Dallas

Quality is central to every process. We use controlled quality procedures to maintain repeatable accuracy from run to run and to ensure finished parts match your design intent.

  • Experienced staff that translates designs into manufacturable solutions.
  • Transparent timelines and responsive updates throughout your manufacturing process.
  • Consistent outcomes that help reduce cost and improve production speed for industrial customers.

Advanced CNC Turning, Milling, And Machining Capabilities

Our facility uses 11-axis equipment to handle complex geometries and tight tolerances. That degree of multi-axis control broadens the machining possibilities for complex components and improves setup efficiency for consistent production runs.

Multi-Axis CNC Machining

Multi-axis control lets us access challenging areas of a part in one setup. Less part repositioning reduce error and improve part consistency.

This machining capability helps produce complex designs and many different materials.

Advanced High-Speed Milling

Fast CNC milling gives clean finishes and fast cycle times. Our team combines high-speed cutting with optimized CAM paths to preserve material quality and satisfy specifications.

Precision Turning Operations

Our CNC turning operations focus on accuracy and surface quality. Each finished part is reviewed to verify dimensions and surface finish.

  • 11-axis equipment for intricate, repeatable results.
  • Fast milling and precision CNC milling for demanding dimensional specifications.
  • Built-in inspection support to ensure manufacturing standards.

Precision Machining For Diverse Industrial Sectors

Lowrance Machine supports industries from energy to aerospace with consistent high-quality manufacturing.

We provide precision machining services for diverse manufacturing markets, including the 21 Fortune 500 companies that call the region home.

The facility’s machining capabilities support essential industries such as energy, aerospace, and other critical industries where reliable machined parts are essential for safety and uptime.

With modern turning and CNC milling machinery, we produce repeatable manufacturing results that meet strict specifications.

  • Accurate production for prototypes and extended runs to keep manufacturing schedules moving.
  • Quality checks that ensure each part conforms to customer requirements.
  • Flexible services to handle unique part geometry and material needs.

Our shop supports a wide range of sectors with the precision production support required to compete. Every machined part is manufactured to meet both performance and quality goals.

Our Commitment To Tight Tolerances And Quality Control

The shop reinforces accuracy with quality systems and continuous process checks. The operation maintains ISO 9000-compliant quality practices and use Statistical Process Control to keep variation low and accuracy high.

SPC And Process Monitoring

Data-based process monitoring maintains process stability and supports reliable part accuracy. Live process charts and control plans show variation trends so problems can be corrected before bad parts are produced.

The shop focuses on high-precision machining expectations so every part satisfies required tolerances. Modern inspection tools verify dimensions and surface finish at critical points in the manufacturing process.

  • ISO 9000 quality systems that support documented procedures and audits.
  • SPC methods that reduce variation and improve efficiency.
  • Measurement routines that validate accuracy across runs.

By combining data-driven process control with experienced staff and calibrated equipment, we minimize waste and deliver consistent, high-quality parts for your industrial projects.

Modern Equipment And Technology Advancements

A stable, climate-controlled 43,000-square-foot facility in Fort Worth gives us the capacity to run sensitive projects with stable results.

Our production floor includes the latest equipment to handle high-accuracy machining and complicated components. Continuous technology improvements maintain efficient and up-to-date manufacturing operations.

We operate as a leading CNC machine shop by investing in tools that improve throughput and lower variation. Those equipment choices create more reliable accuracy and improved quality across each project.

Technology also improves workflows. Modern controls, live monitoring, and automated CAM paths support tight tolerances while helping meet delivery windows.

Equipment Category Key Capability Common Use Benefit
Multi-axis machining centers Difficult geometry Complex production components Reduced setups and stronger consistency
High-speed milling centers High-quality machined finish Short runs and long production runs Faster cycle times
Automatic inspection systems Real-time verification In-process checks Reduced scrap and better quality
Automated tool management Better setup control Recurring production runs Reduced downtime

Streamlined Production And Efficient Lead Times

We shorten schedules without sacrificing quality, helping parts move from design to delivery faster.

The shop operates 20 hours per day from Monday through Friday. The expanded production day shortens lead times while keeping close control on quality.

Rapid Prototyping Support

Rapid prototyping helps convert ideas into real components quickly. Our engineers and operators work together to refine a design and validate function in the first stages of production.

Quick turn models reduce rework and help customers make fast, informed decisions.

Scalable Production Runs

Our process scales from one prototype to full production without abandoning the production method. This repeatable approach preserves precision and keeps costs predictable.

  • Extended 20-hour operating schedules support quicker ramp-up and improved delivery timing.
  • Controlled processes protect consistent quality for both prototype quantities and larger orders.
  • Streamlined workflow helps support reliable CNC machining and on-time output for manufacturing partners.

Secondary Machining And Custom Finishing Options

We provide tailored secondary machining and finishing processes to make sure each component meets functional and visual expectations. Lowrance Machine supports plating, heat treatment, and specialty coatings matched to your material requirements and final application.

We integrate these secondary steps into production so finished machined parts are ready for the next stage. That reduces extra handling and helps speed time to market.

Common finishing services include hardening, passivation, anodizing, and corrosion-resistant coatings. We also provide fine surface finishing for improved appearance and functional wear life.

  • Thermal treatment and hardness profiling for extended durability.
  • Plating and coatings tailored to material and environmental needs.
  • Final machining, deburring, and inspection built into production.
Secondary Service Main Purpose Customer Benefit Common Materials
Heat treatment Improve strength Longer wear performance Steel, alloy
Plating Protection from corrosion Improved part longevity Steel and copper-alloy materials
Protective coatings and finish work Surface appearance & function Improved consistency and finished fit Composites and aluminum

By managing the full chain from precision production to final treatments, we meet specific requirements and deliver high-quality parts you can trust, whether your requirement is appearance-based, performance-based, or both.

Inventory Management And Logistics Solutions

We align delivery schedules to your production rhythm so components show up when your team needs them. This method reduces on-site inventory while keeping assembly lines running.

The Lowrance Machine team provides practical logistics services, including just-in-time delivery and flexible warehousing. Our production team team builds predictable schedules with customers to shorten delivery cycles and stabilize part movement.

Just-In-Time Delivery Support

We coordinate shipments, track orders, and adjust runs to match changing customer demand. This lowers stock levels and reduces carrying costs.

Our planning approach connects cleanly with your manufacturing process. This helps ensure dependable delivery of quality machined parts on the agreed schedule.

Logistics Service Primary Benefit Typical Application
Just-in-time part delivery Lower inventory, less waste Weekly or daily component replenishment
Adaptable warehousing Buffer stock, rapid dispatch Temporary or longer-term storage
Schedule coordination Clearer delivery timing Coordinated manufacturing planning

Expert Team And Manufacturing Experience

Experienced technicians and process engineers work together to convert designs into consistent, high-quality components. The team contributes long-standing industrial manufacturing knowledge to every job and keeps quality consistent across many industries.

Our team pairs skilled talent with current machinery to handle difficult production runs. This combination of staff and equipment helps us meet tight tolerances and maintain steady production for long-term manufacturing partners.

Our capabilities span initial design consultation, fixture development, setup, and final inspection. That complete-service method streamlines project transfer points and limits avoidable rework for clients.

  • Experienced staff who solve technical challenges and optimize process flow.
  • Advanced equipment that supports diverse materials and tight specs.
  • End-to-end services that keep production on schedule and within tolerance.

As an experienced Dallas CNC provider, we hold ourselves to high service and quality standards. The facility remains prepared to produce many types of parts and produce the accuracy your project needs.

Requesting A Quote For Your Custom Parts

Get rapid pricing for parts and production — our team delivers same-day quotes for most requests. Tell us about your part design, material choice, and quantity so we can provide a clear quote quickly.

The shop supports quote requests for turning, milling, and broader machining work. Providing clear requirements allows us to match the right capabilities and return competitive pricing quickly.

  • Fast quote turnaround for prototypes and production quantities.
  • Review design specifications, tolerances, and materials with a knowledgeable team.
  • Faster quoting when you send drawings, volumes, and schedule targets.

Whether your project requires one prototype or a larger production batch, get in touch to move the project forward. The goal is simple quoting that helps your project stay on track.

Final Thoughts

When accuracy matters, our team prioritizes repeatable output that helps support demanding production schedules.

Lowrance Machine remains committed to high quality and precision across every service. We deliver precision machining and CNC machining solutions that meet tight tolerances and maintain accuracy from prototype to production.

Our dependable lead times and controlled processes support many industries in reducing downtime and remaining competitive. Choosing our machining services means working with a provider that values efficient production, clear updates, and on-time results.

Contact us today to discuss how our service can support your next project and keep your parts within spec and on schedule.

Related: Dallas Custom Mold Building Services: From Prototyping to Production

Fiber Secondary Coating Line Design Tips for Long Continuous Runs

Over 70% of new broadband deployments in urban U.S. projects now require fiber-to-the-home. This fast transition toward full-fiber networks highlights the growing need for high-performance production equipment.

FTTH Cable Production Line
Fiber Draw Tower

Shanghai Weiye Optic Fiber Communication Equipment Co (www.weiye-ofc.com) provides automated FTTH cable manufacturing line systems for the U.S. market market. Their turnkey FTTH Cable Production Line for High-Speed Fiber Optics combines machines and control systems. This line turns out drop cables, indoor/outdoor cables, and high-density units for telecom, data centers, and LANs.

This high-performance FTTH cable making machinery provides measurable business value. It enables higher throughput and consistent optical performance with low attenuation. It also aligns with IEC 60794 and ITU-T G.652D / G.657 standards. Customers see reduced labor costs and material waste through automation. Full delivery services cover installation and operator training.

This FTTH cable production line package features fiber draw tower integration, a fiber secondary coating line, and a fiber coloring machine. This system also covers SZ stranding line, fiber ribbon line, compact fiber unit assembly, cable sheathing line, armoring modules, and testing stations. Control as well as power specs commonly rely on Siemens PLC with HMI, operating at 380 V AC ±10% and modular power consumption up to roughly 55 kW depending on configuration.

Shanghai Weiye’s customer support model covers on-site commissioning by experienced engineers, remote monitoring, and rapid troubleshooting. It also provides lifetime technical support and operator training. Clients are usually asked to coordinate engineer logistics as part of standard supplier practice when ordering from FTTH cable machine suppliers.

Core Takeaways

  • FTTH cable line solutions meet growing U.S. demand for fiber-to-the-home deployments.
  • Integrated turnkey packages from Shanghai Weiye combine automation, standards compliance, and operator training.
  • Modular setups use Siemens PLC + HMI and operate near 380 V AC with up to ~55 kW power profiles.
  • Integrated modules cover drawing, coating, coloring, stranding, ribbone, sheathing, armoring, and testing.
  • Advanced FTTH cable making machinery reduces labor, waste, and improves optical consistency.
  • Support includes on-site commissioning, remote diagnostics, and lifetime technical assistance.

SZ stranding lines

FTTH Cable Production Line Technology Explained

The fiber optic cable production process for FTTH calls for precise control at every stage. Manufacturers use integrated lines that combine drawing, coating, stranding, and sheathing. This approach boosts yield and speeds up market entry. It addresses the needs of both residential and enterprise deployments in the United States.

Below, we outline the core components as well as technologies driving modern manufacturing. Each module must operate using precise timing and reliable feedback. This choice of equipment influences product quality, cost, together with flexibility for various cable designs.

Core Components In Modern Fiber Optic Cable Manufacturing

Secondary coating lines apply dual-layer coatings, often 250 µm, using high-output UV curing. Tight buffering and extrusion systems deliver 600–900 µm jackets for indoor together with drop cables.

SZ stranding lines use servo-controlled pay-off and take-up units to handle up to 24 fibers with accurate lay length. Fiber coloring machines use multi-channel UV curing to mark fibers to industry color codes.

Sheathing and extrusion stations form PE, PVC, or LSZH jackets. Armoring units add steel tape or wire for outdoor protection. Cooling troughs and UV dryers stabilize profiles before testing.

Evolution From Traditional To Advanced Production Systems

Early plants used manual as well as semi-automatic modules. Lines were separate, with hand transfers together with basic controls. Advanced facilities move to PLC-controlled, synchronized systems using touchscreen HMIs.

Remote diagnostics as well as modular turnkey setups support rapid changeover between simplex, duplex, ribbon, and armored formats. This transition supports automated fiber optic cable line output and lowers labor dependence.

Key Technologies Driving Industry Innovation

High-precision tension control, based on servo pay-off together with take-up, keeps geometry stable during high-output runs. Multi-zone temperature control using Omron PID as well as precision heaters helps ensure consistent extrusion output quality.

High-speed UV curing and water cooling speed up profile stabilization while reducing energy use. Integrated inline testers measure attenuation, geometry, tensile strength, crush resistance, and aging data.

Process Typical Unit Key Benefit
Optical fiber drawing Automated draw tower with tension feedback Stable core diameter and reduced attenuation
Coating stage UV-curing dual-layer coaters Uniform 250 µm coating for durability
Coloring Fiber coloring unit with multiple channels Reliable color identification for field work
Stranding SZ stranding line, servo-controlled (up to 24 fibers) Accurate lay length across ribbon and loose tube designs
Jacket extrusion & sheathing Energy-saving extruders with multi-zone heaters PE, PVC, or LSZH jackets with tight dimensional control
Cable armoring Steel tape or wire armoring units Improved outdoor mechanical protection
Profile cooling & curing Water troughs and UV dryers Quicker profile setting with fewer defects
Inline testing Inline attenuation and geometry measurement Immediate quality verification and compliance data

Compliance with IEC 60794 and ITU-T G.652D/G.657 variants is standard. Manufacturers typically certify to ISO 9001, CE, and RoHS. These credentials enable diverse applications, from FTTH drop cable production to armored outdoor runs and data center high-density solutions.

Choosing cutting-edge fiber optic line output equipment and modern manufacturing equipment helps firms meet tight tolerances. That decision enables efficient automated fiber optic cable manufacturing and positions companies to deliver on scale as well as consistency.

Essential Equipment In Fiber Secondary Coating Line Operations

The secondary coating stage is critical, giving drawn optical fiber its final diameter and mechanical strength. It prepares the fiber for stranding and cabling. A well-tuned fiber secondary coating line controls coating thickness, adhesion, and surface quality. This protects the glass during handling.

Producers aiming for high-yield, high-speed fiber optic cable production must match material, tension, and curing systems to process requirements.

High-speed secondary coating processes rely on synchronized pay-off, coating heads, and UV ovens. Modern systems achieve high production rates while minimizing excess loss. Precise tension control at pay-off and winder stages prevents microbends and ensures consistent coating thickness across long runs.

Single and dual layer coating applications serve different market needs. Single-layer setups provide basic mechanical protection and a simple optical fiber cable production machine footprint. Dual-layer lines combine a harder inner layer with a softer outer layer to improve microbend resistance and stripability. This helps when fibers are prepared for connectorization.

Temperature control and curing systems are critical to final fiber performance. Multi-zone heaters and Omron PID controllers guide screw/barrel extruders to stable melt flow for LSZH or PVC compounds. UV curing ovens and water trough cooling stabilize the coating profile and reduce variation in excess loss; targets for high-quality single-mode fiber often aim for ≤0.2 dB/km at 1550 nm after extrusion.

Key components from trusted suppliers improve uptime and precision in an optical fiber cable production machine. Extruders such as 50×25 models, screws and barrels from Jinhu, and bearings from NSK are common. Motors from Dongguan Motor, inverters by Shenzhen Inovance, and PLC/HMI platforms from Siemens or Omron provide robust control and monitoring for continuous runs.

Operational parameters shape preventive maintenance and process tuning. Typical pay-off tension ranges from 0.4 to 1.5 N for fiber reels, while radiation as well as curing speeds are adjusted to material type as well as coating thickness. A preventive maintenance cycle around six months keeps secondary coating processes stable and supports reliable high-speed fiber optic cable line output.

Fiber Draw Tower And Preform Processing

The fiber draw tower is the core of optical fiber drawing. This line softens a glass preform in a multi-zone furnace. Then, it pulls a continuous strand with precise diameter control. That step sets the refractive-index profile together with attenuation targets for downstream processes.

Process control on the tower relies on real-time diameter feedback together with tension management. That prevents microbends. Cooling zones and closed-loop systems keep geometry stable during the optical fiber cable production process. Modern towers log metrics for traceability together with rapid troubleshooting.

Output quality supports single-mode fibers such as ITU-T G.652D and bend-insensitive types like G.657A1/A2 for FTTH networks. Draws routinely meet stringent loss figures. Excess loss after coating is kept at or below 0.2 dB/km for high-performance single-mode fiber.

Integration with secondary coating lines requires careful pay-off control. A synchronized handoff preserves alignment and tension as the fiber enters coating, coloring, or ribbon count stations. This link ensures the optical fiber drawing step feeds smoothly into cable assembly.

Equipment vendors such as Shanghai Weiye offer turnkey options. These include testing stations for attenuation, tensile strength, and geometric tolerances. These integrated features help manufacturers scale toward high-speed fiber optic cable production while maintaining ISO-level quality checks.

System Feature Main Purpose Typical Target
Furnace with multiple zones Even preform heating for stable glass viscosity Stable draw speed and refractive profile
Real-time diameter control Preserve core/cladding geometry and lower attenuation Tolerance ±0.5 μm
Managed tension and cooling Prevent microbends and control fiber strength Defined tension by fiber type
Integrated automated pay-off Secure handoff to secondary coating and coloring Synced feed rates for zero-slip transfer
On-line test stations Check attenuation, tensile strength, and geometry Single-mode loss target of ≤0.2 dB/km after coating

Advanced SZ Stranding Line Technology For Cable Assembly

The SZ stranding method creates alternating-direction lays that cut axial stiffness and boost flexibility. As a result, it is ideal for drop cables, building drop assemblies, and any application that needs a flexible core. Manufacturers moving toward automated fiber optic cable manufacturing use SZ approaches to meet tight bend and axial tolerance specs.

Precision in the stranding stage protects optical performance. Current precision stranding equipment relies on servo-driven carriers, rotors, together with modular pay-off racks that accept up to 24 fibers. These systems deliver precise lay-length control together with allow quick reconfiguration for different cable types.

Automated tension control systems keep fibers within safe limits from pay-off to take-up. Servo pay-offs, capstans, together with haul-off units maintain constant linear speed together with target tensions. Typical fiber pay-off tension ranges from 0.4 to 1.5 N while reinforcement pay-offs run between 5 together with 20 N.

Integration with a downstream fiber cable sheathing line streamlines production and reduces handling. Extrusion of PE, PVC, or LSZH jackets at 60–150 m/min syncs with stranding through a Siemens PLC. Cooling troughs and UV dryers stabilize the jacket profile right after extrusion to prevent ovality and reduce mechanical stress.

Optional reinforcement and armoring modules add strength without compromising flexibility. Reinforcement pay-off racks accept steel wires or FRP rods. Armoring units wrap steel tape or wire with adjustable tension to meet specific mechanical ratings.

Built-in consistency control prevents defects before cables leave the line. In-line geometry checks, fiber strain monitors, and optical attenuation measurement detect excess loss or mechanical strain caused by stranding or sheathing. These checks support continuous automated fiber optic cable manufacturing workflows and cut rework.

The combination of a robust sz stranding line, high-end precision stranding equipment, together with a synchronized fiber cable sheathing line delivers a scalable solution for manufacturers. This combination raises throughput while protecting optical integrity as well as mechanical performance in finished cables.

Fiber Coloring Machine And Identification Systems

Coloring and identification are critical in fiber optic cable production. Accurate color application minimizes splicing errors and accelerates field work. Modern equipment combines fast coloring with inline inspection, ensuring high throughput and low defect rates.

Today’s high-speed coloring technology supports multiple channels and quick curing. Machines can operate 8 to 12 color channels simultaneously, aligning with secondary coating lines. UV curing at speeds over 1500 m/min ensures color and adhesion stability for both ribbon and counted fibers.

Below, we discuss standards and coding prevalent in telecom networks.

Color coding adheres to international telecom standards for 12-color cycles and ribbon schemes. Such compliance aids technicians in installation and troubleshooting. Consistent coding significantly reduces field faults and accelerates network deployment.

Quality control integrates advanced fiber identification systems into production lines. In-line cameras, spectrometers, together with sensors detect color discrepancies, poor saturation, as well as coating flaws. This PLC/HMI interface alerts to issues and can pause the line for correction, safeguarding downstream processes.

Machine specifications are vital for uninterrupted runs and material compatibility. Leading equipment accepts UV-curable pigments and inks, compatible with common coatings and extrusion steps. Pay-off reels accommodating 25 km or 50 km spools ensure continuous operation on high-volume lines.

Supplier support is essential for US manufacturers adopting these technologies. Shanghai Weiye as well as other established vendors offer customizable channels, remote diagnostics, as well as onsite training. Such supplier support lowers ramp-up time together with enhances the reliability of fiber optic cable production equipment.

Fiber Solutions For Metal Tube Production

Metal tube together with metal-armored cable assemblies offer robust protection for fiber lines. They are ideal for direct-buried together with industrial applications. This controlled routing of coated fibers into metal tubes prevents microbends, ensuring optical performance remains within specifications.

Processes depend on precision filling and centering units. These modules, in conjunction with fiber optic cable manufacturing equipment, ensure concentric placement and controlled tension during insertion.

Armoring steps involve the use of steel tape or wire units with adjustable tension and wrapping geometry. This method benefits armored fiber cable production by preventing compression of fiber elements. It also keeps reinforcement wires at typical diameters of ø0.4–ø1.0 mm.

Coupling armoring with downstream sheathing and extrusion lines results in a finished outer jacket made of PE, PVC, or LSZH. An optical fiber cable production machine must handle pay-off reels sized for reinforcement and align with sheathing tolerances.

Quality checks include crush, tensile, and aging tests to confirm the armor does not exceed allowable stress on fibers. Standards-based testing ensures long-term reliability in field conditions.

Turnkey solutions from established manufacturers integrate metal tube handling featuring SZ stranding and sheathing lines. These solutions include operator training and maintenance schedules to sustain throughput on fiber optic cable manufacturing equipment.

Buyers should consider compatibility with armored fiber cable production modules, ease of changeover, and service support for field upgrades. These factors reduce downtime and protect investment in an optical fiber cable production machine.

Fiber Ribbon Line And Compact Fiber Unit Production

Advanced data networks require efficient assemblies that pack more fibers into less space. Manufacturers employ a fiber ribbon line to create flat ribbon assemblies for rapid splicing. That line output method employs parallel processes together with precise geometry to meet the needs of MPO trunking and backbone cabling.

Advanced equipment ensures accuracy as well as speed in manufacturing. A fiber ribbon line typically integrates automated alignment, epoxy bonding, precise curing, as well as shear/stacking modules. In-line attenuation as well as geometry testing reduce rework, maintaining high yields.

Compact fiber unit production focuses on tight tolerances and material choice. Extrusion and buffering create compact fiber unit constructions with typical tube diameters from 1.2 to 6.0 mm. Common materials include PBT, PP, and LSZH for durability and flame performance.

High-density cable solutions aim to enhance rack together with tray efficiency in data centers. By increasing fiber count per unit area, these designs shrink cable diameter and simplify routing. They are compatible using MPO trunking together with high-count backbone systems.

Production controls and speeds are critical for throughput. Modern lines can reach up to 800 m/min, depending on configuration. PLC and HMI touch-screen control enable quick parameter changes and synchronization across multiple lines.

Quality and customization remain key differentiators for manufacturers like Shanghai Weiye. Electronic monitoring, customizable ribbon counts, stacking patterns, together with turnkey integration featuring sheathing together with testing stations support bespoke high-output fiber cable line output line requirements.

Key Feature Fiber Ribbon Line Compact Fiber System Benefit To Data Centers
Typical operating speed Up to 800 m/min Typically up to 600–800 m/min More output for large deployment projects
Main production steps Alignment automation, epoxy bonding, and curing Buffering, extrusion, and precision winding Consistent geometry and lower insertion loss
Primary materials Engineered tapes and bonding resins PBT, PP, plus LSZH buffer and jacket materials Durable performance and safety compliance
Quality testing Inline attenuation and geometry checks Tension monitoring and dimensional control Lower failure rates and faster rollout
System integration Sheathing and splice-ready stacking Modular units supporting high-density cable designs Simplified MPO trunking and backbone construction

How To Optimize High-Speed Internet Cables Production

Efficient high-output fiber optic cable production relies on precise line setup together with strict process control. To meet US market demands, manufacturers must adjust pay-off reels, extrusion dies, together with tension systems. This helps ensure optimal output for flat, round, simplex, as well as duplex FTTH profiles.

Cabling Systems Used In FTTH Applications

FTTH cabling systems must accommodate various drop cable types while maintaining consistent center heights, like 1000 mm. Production lines for FTTH include 2- and 4-reel pay-off options. They also feature reinforcement pay-off heads for enhanced strength.

Extruder models, such as a 50×25, control jacket speeds between 100 together with 150 m/min, depending on LSZH or PVC. Extrusion dies for 2.0×3.0 mm profiles guarantee reliable jackets for field installation.

Fiber Pulling Process Quality Assurance

Servo-controlled pay-off and take-up units regulate fiber tension between 0.4–1.5 N to prevent excess loss. Inline systems conduct fiber pull testing, attenuation checks, mechanical tensile tests, and crush as well as aging cycles. That testing regime verify performance.

Key control components include Siemens PLCs together with Omron PID controllers. Motors from Dongguan Motor as well as inverters from Shenzhen Inovance ensure stable operation together with easier maintenance.

Meeting Optical Fiber Drawing Industry Standards

A well-tuned fiber draw tower produces fibers that meet ITU-T G.652D as well as G.657 standards. This goal is to achieve ≤0.2 dB/km excess loss at 1550 nm for high-quality single-mode fiber.

Choosing the best equipment for FTTH cables involves evaluating speed, customization, warranty, and local after-sales support. Top FTTH cable production line manufacturers provide turnkey layouts, remote monitoring, and operator training. Such support reduces ramp-up time for US customers.

Closing Summary

Advanced FTTH cable making machinery integrates various components. These include fiber draw towers, secondary coating, coloring lines, SZ stranding, as well as ribbon units. It also incorporates sheathing, armoring, and automated testing for consistent high-speed fiber manufacturing. A complete fiber optic cable production line is designed for FTTH as well as data center markets. The line enhances throughput, keeps losses low, together with maintains tight tolerances.

For U.S. manufacturers and system integrators, partnering with reputable suppliers is key. They should offer turnkey systems with Siemens or Omron-based controls. This includes on-site commissioning, remote diagnostics, and lifetime technical support. Companies like Shanghai Weiye Optic Fiber Communication Equipment Co provide integrated solutions. These integrated packages simplify automated fiber optic cable manufacturing and reduce time to production.

Technically, ensure line configurations adhere to IEC 60794 and ITU-T G.652D/G.657 standards. Verify tension together with curing settings to meet excess loss targets, such as ≤0.2 dB/km at 1550 nm. Adopt preventive maintenance cycles of roughly six months for reliable 24/7 operation. When planning a new FTTH cable manufacturing line, first evaluate required cable types. Collect product drawings and standards, request detailed equipment specs as well as turnkey proposals, as well as schedule engineer commissioning together with operator training.

Scaling Production with a Modular FTTH Cable Production Line

Could the machines producing fiber optic cable production machinery serve as the unseen force that at last provides true gigabit access to every American home? This article delves into the recent breakthroughs in FTTH Cable Production Line Technology. These advancements are reshaping broadband network infrastructure and accelerating fiber to the home technology across the United States.

Fiber Cable Sheathing Line

Fiber Ribbon Line

Fiber Coloring Machine

Modern advancements in automation, precision engineering, and AI-driven inspection are substantially lowering production costs and improving quality. This synergy makes high-speed internet technology more trustworthy and simpler to implement for service providers and municipalities.

Global optical cable output now exceeds hundreds of millions of kilometers annually. This surge is driven by 5G deployments, hyperscale data centers, and the growing demand for streaming and remote work. The subsequent sections will delve into automation and Industry 4.0, the use of low-loss materials, AI quality control, innovative cable designs such as bend-insensitive fiber and flat drop microcables, and the pursuit of sustainability in production lines.

Telecommunications manufacturing, network planning, and procurement professionals will discover valuable insights. These insights relate to selecting the right fiber optic cable production machinery and optimizing processes. They are designed to meet regional deployment needs and future bandwidth growth.

FTTH Cable Production Line Technology

The term encompasses the machinery, control systems, and materials transforming optical preforms into deployable fiber cables. It covers fiber drawing and coating, SZ stranding, ribbon formation, extrusion of jackets, armoring, taping, automated testing, and final take-up systems. Each step’s precise control defines the fiber optic cable production process, ensuring consistent performance.

The manufacturing chain demands stringent tolerances. SZ stranding systems align dozens of strands with micron-level tension precision. Extrusion lines employ servo-driven extruders and laser micrometers to maintain jacket thickness within ±0.02 mm. Such precision minimizes variability, lowering attenuation and making field splicing easier.

Standards and regulatory frameworks strongly shape manufacturing decisions. Compliance with ITU-T recommendations, such as G.657, and regional fire codes like CPR in Europe, is essential. Meeting these standards ensures products align with the broader broadband network infrastructure.

Quality in production directly impacts network economics and service delivery. Lower attenuation and consistent geometry reduce splice loss and extend reach. This enhances reliability for carriers, ISPs, and utilities, while lowering the total cost of ownership for FTTH deployments. The growing demand for symmetrical multi-gigabit services, 5G backhaul, and data center interconnect is driving the scale-up of modern lines.

Comparing key process components and tolerances reveals their impact on output and quality.

SZ Stranding Line

Manufacturing Stage Standard Control Effect on Performance
Fiber drawing & coating ±1°C temperature control; coating concentricity ±5 µm Consistent geometry; reduced macrobend loss
Ribbon formation and SZ stranding Tension control at micron scale; synchronization to 0.5 ms Consistent fiber pitch; reliable splice and connector behavior
Jacket extrusion and thickness control Laser micrometer feedback; tolerance of ±0.02 mm Uniform protection; more predictable installation handling
Armoring & taping Servo-controlled feed rate; layer alignment control Better crush resistance; meets aerial and underground specs
Automated testing & take-up OTDR and insertion loss checks at line speed; tension-controlled winding Fully traceable quality; less rework and fewer field failures

Manufacturers like Corning, Prysmian Group, and Sumitomo Electric focus on tighter process control to meet operator expectations. Continuous advancements in the fiber optic cable production process enable networks to scale while maintaining performance in the last mile of broadband network infrastructure.

Automation And Industry 4.0 In Fiber Optic Cable Production

Factory floors for fiber optic cable production machinery now mirror advanced manufacturing plants from other industries. Smart controls, synchronized stages, and data-driven decision making raise output and protect quality. These shifts shorten commissioning time for new product families. They let telecommunications equipment manufacturers pivot between armored aerial lines and microcable runs with minimal downtime.

Smart machinery and PLC integration

Programmable logic controllers coordinate stranding frames, ribbon formers, and take-up units to keep tension within sub-0.01mm windows. Servo-driven extrusion coupled with laser micrometers enforce ±0.02mm jacket thickness. The result is fewer rejects, less rework, and consistent optical performance on every reel.

Edge computing and process orchestration

Local edge servers ingest terabytes of telemetry each day. They drive low-latency closed-loop adjustments and push immediate alerts when deviations occur. This approach keeps optical fiber cable equipment running at peak efficiency. It supports real-time quality assurance during long production runs.

AGVs, material handling, and workflow gains

Automated Guided Vehicles move heavy cable drums with millimeter-level repeatability. Laser-navigated AGVs reduce manual handling injuries and speed material flow between extrusion, curing, and drum stations. This automation lowers labor costs while raising throughput on ftth cable production line technology setups.

Benefits for manufacturers and the supply chain

  • Higher throughput with repeatable results
  • Quicker prototyping and a shorter path to market
  • Lower labor exposure and reduced operating cost
  • Better integration between optical fiber cable equipment and enterprise systems

Adoption across the industry ecosystem

Leading telecommunications equipment manufacturers pair PLCs with robotic arms, AGVs, and industrial IoT stacks to reach Industry 4.0 goals. This integration creates a resilient production base. It is able to adapt as demand shifts toward denser, more complex FTTH offerings.

Precision Engineering Breakthroughs For Lower Attenuation

Advances in materials and mechanical design are driving down loss in modern fiber lines. Engineers pair ultra-low loss fiber with tighter coating control to reduce intrinsic and bending attenuation. These gains matter to network operators who want longer spans and fewer amplifiers in high-speed internet technology deployments.

The fiber optic cable production process now favors smaller coated diameters such as 180µm and 160µm. These sizes let manufacturers increase fiber count and build denser microcables without sacrificing handling or optical stability.

Low-Loss Glass And Advanced Coatings

Manufacturers use improved glass formulations that lower Rayleigh scattering and reduce baseline attenuation. Ultra-low loss fiber variants extend reach for long-haul and high-capacity links while easing repeaters and amplifier requirements.

Coating chemistry has progressed too. UV-cured acrylate systems cut microbending loss by roughly 40% compared with earlier generations. That performance drop helps maintain signal integrity in cramped ducts and tight bends common in FTTH and 5G backhaul networks.

Central Strength Members And Mechanical Design

Mechanical design updates center on robustness and dimensional control. Fiber-reinforced plastic (FRP) rods with tensile strengths near 1.2 GPa serve as central strength members. They limit elongation during pulling and boost crush and bending resilience.

Water-blocking advances use swellable yarns and grease-free gel compounds to achieve near-complete moisture resistance. These measures protect optical paths and raise in-service reliability for cable installations in challenging environments.

These precision engineering steps integrate directly into fiber optic cable manufacturing workflows. When the production line aligns glass, coating, and mechanical specs, attenuation falls and networks gain reliability. That alignment shortens time to service for operators deploying modern broadband and high-speed internet technology.

Quality Control 4.0 And AI-Powered Inspection

Smart factories for fiber optic cable production now embed inspection systems that run continuously. These systems combine machine vision, machine learning, and automated testers to watch every reel and spool. The result is tighter feedback during the fiber optic cable production process and fewer surprises in the field.

AI models score coating uniformity, microbends, and surface defects at line speed. They cross-reference process telemetry from fiber optic cable production machinery and predict deviations hours before a reel moves to final spooling. This allows for in-line adjustments without stopping the line.

Automated OTDR integration performs 100% attenuation testing on every length. Modern OTDR systems using 1550nm sources map loss across reels and flag changes as small as 0.01 dB/km. Inline OTDR logs feed edge analytics for rapid root-cause tracing when a batch shows anomalies.

Robotic bend-radius simulators apply repeated stress cycles while monitoring macrobend loss. These testers validate compliance with ITU-T G.657 and customer bend specifications by running controlled bends at multiples of the cable diameter. Test outcomes are tied to batch IDs for traceability.

Thermal cycling chambers stress jackets and splices across wide temperature ranges. Environmental tests up to +85°C and down to -60°C confirm stability for extreme climates. Automated logs record each chamber run and link results to production lots.

Quality control 4.0 reduces returns and field failures by making 100% in-line testing routine. Edge analytics and OTDR integration shorten diagnosis times and improve regulatory compliance. Broadband operators see fewer truck rolls and better lifecycle performance for FTTH networks.

Cable Design Innovations For FTTH Deployments

New cable designs address common field challenges in fiber to the home technology. Engineers focus on durability, space economy, and speed of activation. These trends reduce installation time and lower long-term operational costs.

Bend-Insensitive Fiber Benefits For MDUs And Tight Routing

Bend-insensitive fiber maintains signal strength when routed around corners and through confined spaces. ITU-T G.657 compliant fibers minimize attenuation at tight radii, protecting links in multi-dwelling units and behind baseboards. Prysmian’s BendBright family and BendBrightXS exemplify how smaller coated diameters facilitate routing without compromising optical performance.

Flat Drop And Microcable Options For Flexible Deployments

Flat drop cable remains a preferred choice for aerial self-support, duct installs, and direct burial in North America. Its profile accommodates narrow pathways and enhances aerial spans with appropriate clamps. High-fiber-count flat drops necessitate enhanced radial strength and more robust hardware for longer spans.

Microcable technologies reduce outside plant profiles to 8 mm or less. Microcables and air-blown systems enable capacity addition inside existing ducts and congested corridors. These approaches reduce civil works, lower labor costs, and facilitate incremental network growth for urban and campus builds.

Pre-Connectorized Solutions To Speed Field Activation

Pre-connectorized solutions offer factory-terminated, plug-and-play assemblies that minimize field fusion and connector errors. Hardened outdoor connectors and vendor offerings like Prysmian’s ezDROP simplify mass rollouts and enhance first-pass yield. Service teams experience fewer truck rolls and faster service turn-up for smart city and 5G edge projects.

Cable Design Core Advantage Typical Application Key Deployment Consideration
Bend-insensitive optical fiber Reliable performance at tight radii Multi-dwelling units, indoor routing, compact pathways Choose ITU-T G.657 variants for indoor runs
Flat drop cable Flexible installation options Aerial drops, direct burial, duct insertion Apply suitable clamps and radial-strength hardware
Microcable solutions Compact profile with scalable capacity Microduct installations, crowded urban ducts Air-blown systems require compatible blower tools
Pre-connectorized solutions Faster service turn-up and reduced errors Large deployments, rapid activation Plan for standardized connector interfaces

Sustainability And Energy Efficiency In Production Lines

Manufacturers in the fiber optic cable industry are embracing greener practices to reduce costs and meet consumer demands. Facilities prioritizing sustainable production witness improvements in operational efficiency and brand reputation. These advancements impact power systems, cooling, raw materials, and waste management.

Energy recovery strategies are becoming prevalent on extrusion lines and take-up reels. Regenerative braking on motor-driven spools returns power to the grid, thereby lowering net consumption. Studies indicate that energy recovery can reduce drive energy use by up to 32 percent in retrofitted reels.

Closed-loop cooling and chiller-less extrusion systems are reducing water demand. Adiabatic cooling can decrease water use by as much as 75 percent, particularly beneficial in water-scarce areas. Plants employing closed-loop cooling systems, in conjunction with heat exchangers, maintain temperature control while reducing utility expenses.

Recyclable jacket materials are transforming the disposal of cables. New polypropylene-based and modified polymer compounds meet mechanical and fire-safety standards, enabling higher recycling rates. Suppliers like Borealis and LyondellBasell are developing compounds that support the circular economy in cable jackets.

Process optimization minimizes scrap before recycling. Precision extrusion, in-line laser measurement, and real-time analytics reduce off-spec runs. Digital twins enable engineers to refine parameters, enhancing batch yields and reducing material waste.

Regulatory pressures and corporate ESG goals are compelling operators to favor vendors with transparent sustainability metrics. Municipal procurement teams and large network operators increasingly consider lifecycle impacts when selecting suppliers.

Operational Area Typical Gain Key Benefit
Take-up reels with regenerative drives As much as 32% lower energy use Reduced electricity costs and lower peak demand
Closed-loop cooling and adiabatic systems Water use reduced by ~75% Lower water bills and compliance in arid regions
Recyclable outer-jacket materials Greater post-consumer recyclability Better circularity and simpler end-of-life handling
Inline inspection and digital twins Noticeable double-digit reductions in scrap and off-spec output Better yield, less material waste
Reporting and sustainability certifications Improved procurement positioning Competitive advantage with network operators

Implementing these measures enhances the resilience of fiber optic cable manufacturing. It leads to lower lifecycle costs and easier compliance. Manufacturers integrating energy recovery and recyclable jacket materials position themselves for growth in the green procurement market.

Emerging Technologies Shaping Cable Manufacturing

New technologies are transforming the design and operation of fiber optic cable production machinery. These innovations expedite commissioning, diminish prototyping cycles, and empower manufacturers to test process alterations without halting production.

Digital twins create virtual replicas of entire production lines and novel cable designs. Engineers at Corning and Prysmian leverage these models to validate footprint, material flow, and layout before physical construction. Studies indicate commissioning can be up to 60% swifter when teams execute virtual scenarios and optimize layouts beforehand.

Digital twins facilitate expedited R&D for bespoke items such as armored variants and anti-rodent jackets. Virtual testing minimizes the necessity for physical prototypes and accelerates market entry. Teams can simulate process modifications, observe material interactions, and refine equipment parameters in a risk-free milieu.

AI systems introduce predictive capabilities on the factory floor. Machine learning scrutinizes 50+ parameters to forecast failures and quality deviations hours in advance. This AI predictive maintenance lessens unplanned downtime and elevates overall equipment effectiveness for high-volume lines.

Manufacturers like Siemens and ABB integrate AI with edge computing, enabling models to operate proximal to machines. Alerts prompt targeted inspections, spare part staging, and corrective actions before a fault halts production. This strategy maintains yield and shortens mean time to repair.

Quantum fiber sensing and distributed monitoring extend capabilities beyond production to the deployed cable. Embedded Brillouin and distributed acoustic sensing provide continuous strain and temperature data across extensive spans.

Integration of quantum fiber sensing enhances network diagnostics and supports structural health monitoring. Field teams acquire actionable insights when sensing data is linked to manufacturing records and test logs. This connection enables tracing anomalies to specific production batches.

Combined workflows—digital twins plus AI predictive maintenance—accelerate both commissioning and product development. Manufacturers embracing these tools can respond more swiftly to market fluctuations and deliver higher-value, differentiated cables.

Market-Driven Production Adaptations And Regional Needs

The global demand for fiber access compels manufacturers to adapt their production lines to local requirements. Regional fiber optic cable manufacturing now emphasizes durability, density, and safety. Plants employ modular equipment, enabling swift transitions between product families and meeting specific operator needs without significant delays.

In North America, networks predominantly opt for aerial routes and robust outside-plant solutions. Producers concentrate on creating armored aerial cables with enhanced breaking strength, corrosion-resistant armor, and simplified pole-mount installation. These designs withstand wind, ice, and long span stresses typical of utility corridors.

North American Priorities: Aerial And Armored Designs

Armored aerial cables are engineered for enduring reliability on poles and open spans. They boast 1,200 lb or greater tensile ratings and integrated steel or aluminum armoring to safeguard fibers against mechanical damage. Manufacturers deploy modular armoring units and rapid testing rigs, enabling mass production of these variants.

APAC And Europe: High-Density Microcables And Regulatory Compliance

In APAC, the scarcity of space and the need for dense builds drive demand for high-density microcables. These cables feature compact stranding towers and reduced-diameter fiber stacks, allowing for more fibers per duct. They significantly reduce civil costs by facilitating quicker overbuilds and easier microtrenching.

Europe mandates strict regulatory compliance for buildings and public spaces. Producers offer halogen-free, flame-retardant jackets that meet CPR classes like B2ca. Compliance testing is integrated into production lines, ensuring products meet fire-safety rules for indoor and outdoor applications promptly.

Across regions, the ability to adapt production is paramount. Compact stranding towers, modular extrusion and armoring units, and rapid prototyping enable factories to switch from armored aerial cables to microcable runs in mere hours. This flexibility allows operators to fulfill unique specifications while adhering to local codes.

Case Studies And Manufacturer Spotlight: Shanghai Weiye OFC Equipment

Shanghai Weiye OFC Equipment has solidified its reputation as a leading telecommunications equipment manufacturer. They cater to the FTTH and broader fiber markets. Their optical fiber cable equipment boasts advanced features, including SZ stranding, ribbon production, and extrusion with servo control. This ensures tight tolerances and high yields.

Their machinery for fiber optic cable production is equally impressive. It includes tape armoring units, automated take-up reels with regenerative drives, and integrated OTDR and vision inspection stations. These systems support various applications, such as bend-insensitive fiber, microcables, and pre-connectorized solutions. These are crucial for FTTH, 5G backhaul, and dense urban deployments.

Quality and sustainability are integral to their offerings. They employ OTDR testing, AI-powered inspection, and robotic bend simulators to meet QC 4.0 standards. Additionally, energy recovery options and closed-loop cooling reduce operating costs and scrap. Modular designs with AGV and edge computing support enable rapid reconfiguration and digital twin commissioning, catering to U.S. manufacturers and contract producers.

For operators in the United States, investing in Shanghai Weiye OFC Equipment can significantly enhance production capabilities. It ensures compliance with strict attenuation and mechanical specifications. This accelerates the introduction of new cable families, vital for broadband expansion. The company’s systems harmonize technical performance with practical manufacturing requirements.

FAQ

Q: What Advances Define Modern FTTH Cable Production Line Technology?

A: Modern FTTH cable production lines integrate high-precision mechanical systems with servo-driven extrusion. They utilize SZ stranding and ribbon machines, along with automated take-up reels. These systems also include integrated OTDR and AI-driven vision inspection, PLC orchestration, AGV material handling, and edge computing. Such advancements enable micron-level tension control and ±0.02mm jacket thickness tolerances. They achieve 95%+ automation and 100% in-line testing, reducing attenuation, scrap, and time-to-market.

Q: How Do You Define The Scope Of FTTH Cable Production Line Technology?

A: FTTH cable production line technology includes the machinery, process controls, and materials for fiber-to-the-home networks. It includes optical fiber drawing and coating, SZ stranding, and ribbon formation. Extrusion of inner and outer jackets, armoring or taping modules, and automated take-up and drum handling are also part of it. In-line optical and mechanical testing, along with the software stack—PLCs, edge servers, and industrial IoT—are integral to the process.

Q: Why Does Production-Line Quality Matter For Broadband Network Infrastructure?

A: Production-line quality directly impacts attenuation, splice loss, mechanical robustness, and long-term reliability. High-precision manufacturing minimizes intrinsic and macrobending losses. It extends reach, lowers field interventions, and improves first-pass yields. For carriers and ISPs, this translates to fewer truck rolls, lower total cost of ownership, and higher service availability for high-speed internet, 5G backhaul, and symmetrical multi-gigabit home services.

Q: What Role Do PLCs And Smart Machinery Play In Industry 4.0 Production Lines?

A: Programmable logic controllers (PLCs) provide deterministic synchronization across SZ stranding, ribbon forming, and take-up units. They enable sub-0.01mm tension precision, closed-loop extrusion control, automated recipe changes, and safety interlocks. When combined with robotic arms and automated armoring modules, PLCs form the backbone of Industry 4.0 production. They drive repeatability and high throughput with minimal human intervention.

Q: How Are AGVs And Edge Computing Used On Modern Cable Production Floors?

A: Laser-navigated AGVs move heavy drums and material spools with high positioning accuracy. Industry examples show 1,200kg capacity and sub-5cm placement. Edge computing processes terabytes of telemetry locally, delivering low-latency analytics and real-time quality alerts. Together, AGVs and edge computing improve material flow, reduce manual handling risks, and enable rapid correction of process deviations.

Q: What Precision Engineering Improvements Reduce Optical Attenuation?

A: Improvements include ultra-low-loss (ULL) glass formulations and advanced UV-cured acrylate coatings. These coatings cut microbending losses. Smaller coated diameters (e.g., 160–180µm) enable denser cable designs. Tight control of drawing tension, coating cure profiles, and extrusion concentricity—monitored by laser micrometers and closed-loop controls—lowers intrinsic loss and fluctuation across production reels.

Q: How Do Central Strength Members And Mechanical Design Affect Cable Performance?

A: Mechanical designs incorporating fiber-reinforced plastic (FRP) rods or high-strength central members control elongation during installation. They resist crush and bending, protecting fiber glass from strain. Proper selection of strength elements and buffer constructions reduces installation-induced loss, improves long-term reliability, and supports aerial or duct deployments with demanding mechanical requirements.

Q: What Does “QC 4.0” Mean And How Is It Implemented?

A: QC 4.0 describes a fully instrumented, data-driven quality-control regime. It includes 100% in-line testing, AI-powered vision inspection, automated OTDR mapping, robotic bend tests, and environmental chambers integrated into the production workflow. Edge analytics, traceable test logs, and predictive models enable rapid root-cause analysis, minimize returns, and ensure compliance with ITU-T and operator specifications.

Q: How Is OTDR Testing Integrated Into Production And What Sensitivity Can It Achieve?

A: Automated OTDR stations are integrated inline or at take-up to perform full-length attenuation mapping. They use dual-wavelength sources (including 1550nm). Modern setups can detect variations down to 0.01 dB/km, map localized defects, and tie results to batch IDs for traceability. This enables manufacturers to flag and quarantine reels before shipment, improving field reliability.

Q: What Are Robotic Bend-Radius Simulators And Thermal Cycling Chambers Used For?

A: Robotic bend-radius simulators apply repeated controlled bends and record macrobend loss to verify compliance with ITU-T G.657 and customer specs. Thermal cycling chambers run jackets and assemblies through −60°C to +85°C cycles to validate dimensional stability, jacket adhesion, and splice performance under extremes. Automated test logs provide traceable evidence for operator and regulatory requirements.

Q: What Cable Design Innovations Are Most Relevant To FTTH Deployments?

A: Key innovations include bend-insensitive fiber (BIF) for tight routing in MDUs and indoor paths. Flat drop and high-fiber-count flat assemblies are used for aerial and direct-burial North American use cases. Microcables and air-blown systems are for duct-constrained environments. Pre-connectorized assemblies speed field activation and reduce termination errors.

Q: Why Is Bend-Insensitive Fiber Important For MDUs And Tight Routing?

A: Bend-insensitive fiber maintains low loss under tight radii and repeated handling. It is crucial in multi-dwelling units, plenum runs, and behind baseboards. ITU-T G.657-compliant fibers help prevent macrobending loss during installation and reduce service calls related to routing-induced degradation. They support denser routing with fewer installation constraints.

Q: How Do Flat Drop Cables And Microcables Differ In Deployment Benefits?

A: Flat drop cables offer flexible aerial and direct-burial deployment with compact profiles suited to service drops. Microcables (≤8mm) and microduct systems excel in congested ducts and enable incremental capacity growth via air-blown installation. Choice depends on regional deployment practice, span requirements, and operator preferences.

Q: What Advantages Do Pre-Connectorized Solutions Provide?

A: Factory-terminated, hardened pre-connectorized assemblies reduce field splicing, eliminate human termination variability, and speed up service activation. They improve first-pass yield. Products like hardened OptiTap-style connectors and vendor pre-terminated drops support rapid mass-deployment strategies and lower workforce training needs.

Q: How Are Energy Recovery And Cooling Innovations Improving Sustainability?

A: Regenerative drives on take-up reels and motor assemblies can capture braking energy, reducing net consumption by industry-reported amounts (example: up to ~32%). Chiller-less or adiabatic extrusion cooling reduces water use by up to 75%. These measures lower operational cost, reduce water consumption, and align production with corporate sustainability targets.

Q: Are Recyclable Jacket Materials And Waste Reduction Practical For Production?

A: Yes. Recyclable compounds such as specially formulated polypropylene-based jackets can meet mechanical and flame performance while improving end-of-life recycling. Precision extrusion and in-line inspection reduce scrap rates. Combined with material-efficient tooling and digital-twin optimization, manufacturers can materially lower waste and support circular-economy goals.

Q: What Role Do Digital Twins Play In Cable Manufacturing?

A: Digital twins create virtual replicas of production lines and cable designs to simulate process changes and validate material flow. They accelerate commissioning. Industry estimates show commissioning and prototyping time reduced significantly (case examples up to ~60%). Digital twins also support offline testing of recipe changes and faster roll-out of new product families.

Q: How Does AI Enable Predictive Maintenance And Quality Prediction?

A: Machine learning models trained on dozens of production parameters can forecast equipment faults hours in advance and predict quality drift. Predictive maintenance reduces unplanned downtime, improves OEE, and allows planned service windows. AI-driven quality models provide early alerts for deviations that would otherwise produce rejects or field failures.

Q: What Is The Significance Of Quantum And Distributed Sensing Integration In Cables?

A: Embedding distributed sensing capabilities—such as Brillouin-based strain sensing and distributed acoustic sensing (DAS)—adds network-level telemetry for structural health monitoring, intrusion detection, and environmental diagnostics. Integrating sensing into cable designs enables added-value services and improved operational visibility for carriers and critical infrastructure owners.

Q: How Do Production Lines Adapt To Regional Market Needs (North America, APAC, Europe)?

A: Lines are modular and reconfigurable to meet regional priorities. North America focuses on robust aerial and armored designs with higher breaking-strength requirements for pole deployments. APAC emphasizes high-density microcables and compact stranding for dense urban rollouts. Europe prioritizes halogen-free flame-retardant jackets and CPR fire-class compliance. Modular stranding towers, quick-change extrusion heads, and configurable armoring units enable fast changeovers.

Q: What Manufacturing Equipment Is Essential To Support Varied FTTH Product Families?

A: Essential equipment includes SZ stranding machines (dozens to hundreds of fibers with micron-level tension control), ribbonization lines, servo-driven extruders with laser micrometers, tape or armor-wrapping stations, automated take-up reels with regenerative drives, inline OTDR and AI vision inspection, AGV drum handling, and edge computing/PLC orchestration for Industry 4.0 integration.

Q: How Do Manufacturers Ensure Compliance With Standards Like ITU-T G.657 And Regional Safety Codes?

A: Compliance is ensured via precise material selection (bend-insensitive fiber types), controlled production recipes, automated in-line tests (OTDR, macrobend testers), and environmental qualification (thermal cycling, flame tests). Traceable test logs, batch IDs, and documented QC protocols align production outputs with ITU-T recommendations and regional regulations such as CPR classifications in Europe.

Q: What Benefits Can U.S. Manufacturers Expect From Equipment Suppliers Like Shanghai Weiye OFC Equipment?

A: Suppliers like Shanghai Weiye provide modular, Industry 4.0-ready production machinery—SZ stranding, ribbon lines, precision extrusion with closed-loop controls, AI inspection modules, and integrated OTDR testing. This enables U.S. contract manufacturers and in-house producers to scale FTTH output, maintain tight attenuation and mechanical tolerances, adopt sustainability options (energy recovery, closed-loop cooling), and shorten time-to-market for variants such as armored aerial, flat drop, microcable, and pre-connectorized assemblies.

Q: How Do In-Line AI Inspection Systems Detect Subtle Defects At Production Speed?

A: AI-powered machine vision inspects coating uniformity, surface defects, and microbends using high-resolution cameras and convolutional models trained on labeled defect libraries. Models correlate dozens of parameters—diameter variance, coating texture, micro-crack signatures—to predict deviations hours before they become out-of-spec reels. This enables automated rejection, parameter adjustment, and reduced downstream field failures.

Q: What Testing Sensitivity And Traceability Are Achievable For Attenuation And Mechanical Validation?

A: Modern production lines integrate automated OTDR systems capable of resolving 0.01 dB/km changes, robotic bend simulators for repeated macrobend stress testing, and thermal chambers for extreme environment validation. Test results are stored with batch and reel identifiers in edge or cloud databases, providing full traceability for operator acceptance, regulatory audits, and customer service diagnostics.

Q: How Do Production Innovations Translate Into Market Outcomes For Network Operators?

A: Innovations in manufacturing yield lower-loss fibers, denser cable designs, and factory-terminated assemblies that reduce installation time and errors. Operators benefit from higher service reliability, fewer truck rolls, lower lifecycle costs, and faster rollout of symmetrical multi-gigabit services. These outcomes support widespread FTTH adoption, 5G backhaul capacity, and scalable connectivity for smart cities and hyperscale data center interconnects.

Related: Training Your Workforce on Next-Gen Fiber Cable Sheathing Line Software